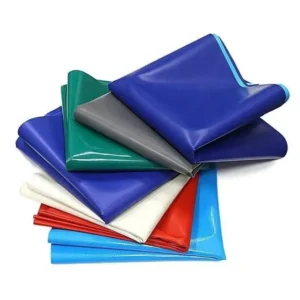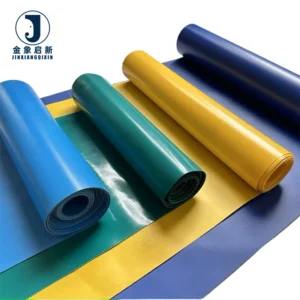
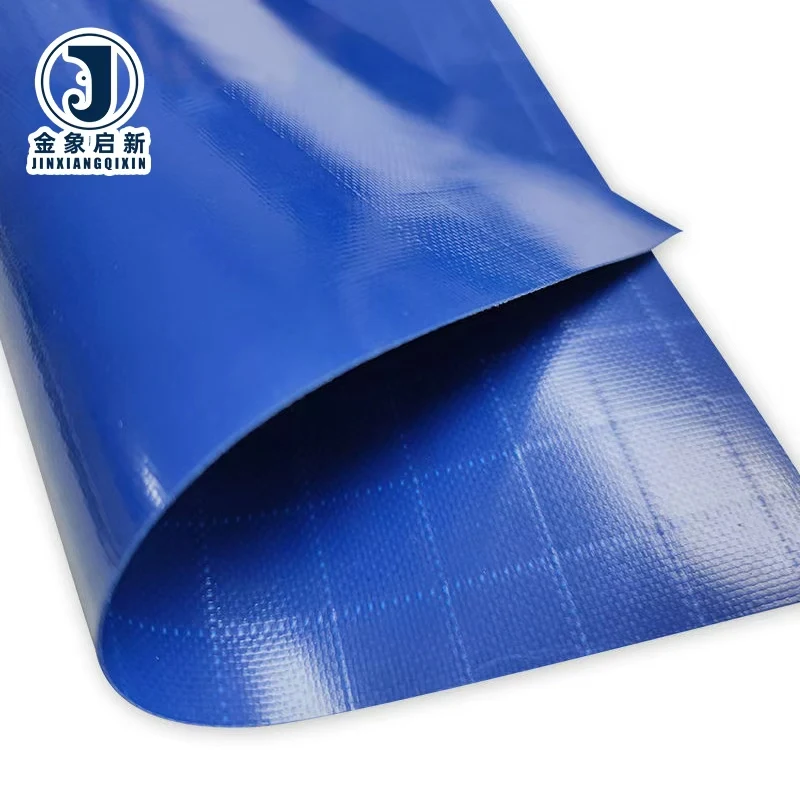
Coating Consistency Control — Every roll of PE Tarpaulin Roll material and coating undergoes stage-by-stage lamination monitoring to ensure the HDPE weave and LDPE film bond remains intact across the full width and length, verified before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PE Tarpaulin Roll with Anti-static – Laminated |
| Base Fabric | HDPE weaving |
| Coating Method | LDPE lamination on both sides |
| GSM Range | 50 g/m² ~ 300 g/m² |
| Total Thickness | 0.2 – 0.4 mm (8 mil – 16 mil) |
| Weave Density Options | 6×6, 6×7, 7×7, 7×8, 8×8, 9×9, 8×10, 10×10, 12×12, 14×14, 14×16 |
| Color Options | Blue, Blue/Orange, Green, Grey, Black, Clear, Grey/Green, Orange, or custom |
| Roll Width Options | 6 ft, 8 ft, 10 ft, 12 ft / 2 m, 4 m, 6 m / Custom |
| Roll Length Options | 100 yards, 100 meters, or custom |
| Anti-static | Claimed in title (grade not stated in source — confirm grade required for your application) |
| UV Treatment | Available (test basis not stated — request test report for your market) |
| Waterproof | Yes |
| Anti-Mildew | Yes |
| Key Features | Waterproof, washable, tear resistant, weather proof, anti-aging |
| Standards | ISO, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Truck and trailer covers | Road abrasion, flex stress at tie-down points, sustained UV and weather exposure |
| Construction material covers | Dust and debris impact, outdoor storage, scaffold wrapping with wind load |
| Agricultural stock protection | Rain ingress prevention, prolonged sun exposure, mildew risk under humidity |
| Industrial equipment wrapping | Static-sensitive environments, repeated handling and folding, contact with oils |
| Home and garden canopies | Moderate UV, intermittent rain, seasonal setup and teardown cycles |
Why Coating Weight Matters More Than GSM on a PE Tarpaulin Roll
LDPE lamination thickness and adhesion quality determine long-term waterproof integrity, not the GSM figure printed on the label.
Technical buyers sourcing PE tarpaulin often receive rolls where the stated GSM does not survive a simple scale-and-measure check on arrival. The discrepancy usually traces to thinner-than-quoted lamination on one or both sides, which leaves the HDPE base fabric exposed at weave intersections. Once water penetrates those micro-gaps, the fabric delaminates from the inside outward, and the failure is rarely caught until the tarp is already deployed over a load [NEED_CITE: material verification methods for laminated tarpaulin rolls per ISO testing frameworks]. A specification sheet that separates base fabric weight from coating weight per side eliminates this guesswork.
Base Fabric Density and Its Effect on Tear Propagation
The HDPE weave density directly governs how a tear initiates and spreads once the fabric is punctured. A 6×6 weave at the lighter GSM grades provides adequate coverage for short-term agricultural or construction use, while a 14×14 or 14×16 mesh produces a denser grid that resists tear extension under wind load and mechanical stress. PE Tarpaulin Roll material and coating performance hinges on selecting the correct mesh count for the anticipated exposure, not simply choosing the heaviest option available. Denser weaves also distribute lamination pressure more evenly during the LDPE bonding stage, reducing the risk of pinhole defects.
Lamination Adhesion and Flex-Point Behaviour
LDPE lamination on both sides of the HDPE base fabric creates a fully encapsulated sheet, but the bond strength at the interface determines how the fabric behaves at fold lines and flex points. When a laminated PE tarp is folded repeatedly — as happens with truck covers that are removed and restowed — the lamination can micro-crack along the fold axis if adhesion was insufficient during production. This is distinct from knife-coated PVC where the coating penetrates the yarn bundle; lamination sits on the surface, making process control during the heating and pressure stage critical [NEED_CITE: coating adhesion test methods for laminated polyethylene fabrics]. Specifying the lamination weight per side, rather than only the total GSM, gives fabricators a reliable basis for predicting flex durability.
How Weave, Thickness and Coating Interact in Practice
The 0.2–0.4 mm thickness range spans from light-duty covers to medium-duty industrial wraps, but thickness alone does not predict tensile performance. A 0.35 mm sheet built on a 7×7 weave with heavy lamination may tear more easily than a 0.25 mm sheet on a 12×12 weave with balanced lamination, because the base fabric — not the coating — carries the tensile and tear load. The LDPE lamination primarily provides waterproofing and UV shielding (where treatment is applied), while the HDPE yarn denier and mesh count supply structural strength. Understanding this division of function allows specifiers to match PE Tarpaulin Roll material and coating grades precisely to the mechanical demands of each application. For anti-static environments, confirm the additive grade with the supplier before committing to a production run, as the required dissipation rate varies by market and application.
The Hidden Cost of Specifying on Price Per Kilogram Alone
When rolls are procured on a cost-per-kilogram basis without locking down weave density and lamination weight separately, the incentive structure favours thinner lamination on a heavier base yarn to hit the target GSM cheaply. The result arrives looking correct on a weight check but fails prematurely because the coating is too thin to bridge the weave gaps under sustained weather exposure. Colour variation between rolls in the same shipment compounds the problem when tarps are installed side by side on a scaffold or truck fleet — a visible mismatch that triggers rejection and rework [NEED_CITE: batch colour consistency standards for laminated tarpaulin production]. Specifying mesh count, lamination weight per side, and colour reference together eliminates both structural and cosmetic failure modes.
Why Procurement Teams Source PE Tarpaulin Roll Material and Coating Here
Three full production lines with 36 sets of lamination equipment support bulk roll output with consistent coating weight across the web width. A 10-person R&D team develops samples within days for custom GSM, weave density, and colour requirements, allowing buyers to validate material before committing to container volume. Dedicated QA and QC checkpoints at each production stage — yarn extrusion, weaving, lamination, and winding — ensure the specification sheet matches what ships. Pre-shipment inspection covers roll-by-roll GSM verification and visual checks for lamination defects. Roll widths up to 6 m and lengths to 100 meters or custom reduce splice counts for large-format fabricators. Documentation packages include material data, test reports where applicable, and customs-ready paperwork for export.
Documentation & Verification
- Material specification sheet stating HDPE weave count, LDPE lamination weight per side, and total GSM
- UV treatment test report provided when anti-UV grades are specified for the order
- Pre-shipment inspection record with GSM verification measured per roll against the quoted value
- ISO and CE certificates available on request, linked to the production batch
- Roll packing list detailing width, length, colour reference, and net weight per roll
Fabrication, Handling & Storage
- Heat-weld parameters depend on LDPE coating thickness; confirm temperature and dwell time for the 0.2–0.4 mm range before production
- PP rope reinforced hems with galvanised eyelets distribute load at tie-down points on finished tarpaulins
- Store rolls upright on end caps to prevent flat-spot deformation across the LDPE lamination surface
- Unroll and allow the fabric to relax at ambient temperature before cutting to reduce dimensional drift
- Custom brand printing adhesion depends on the surface finish; request a print sample for the selected colour before bulk run
What to Include in Your Inquiry
Provide the end-use application, anticipated exposure conditions, and the specific anti-static or UV grade your market requires. State the roll width, GSM range, and weave density you need, along with annual volume and colour references. Indicate whether you require raw roll stock or finished tarpaulins with eyelets and hems, and confirm if pre-production samples are needed for engineering approval.
Frequently Asked Questions
Q: How can I verify the GSM of PE tarpaulin rolls on arrival?
A: Cut a measured sample from the roll — for example, a 1 m × 1 m square — and weigh it on a calibrated scale. Compare the result to the GSM stated on the material specification sheet. Discrepancies typically indicate thinner LDPE lamination than quoted. We provide a pre-shipment inspection record with per-roll GSM data so you can cross-check immediately upon receipt.
Q: What does mesh count tell me about the strength of a PE tarpaulin?
A: Mesh count describes the number of HDPE warp and weft yarns per unit area. A denser weave such as 14×14 resists tear propagation better than a 6×6 at equivalent GSM because the load distributes across more yarn intersections. The LDPE lamination contributes waterproofing but does not carry tensile load, so the base weave density is the primary structural variable.
Q: Is there a test report available for anti-UV treatment?
A: UV treatment is available across our PE tarpaulin range, but the specific test basis and exposure rating depend on the additive package selected for your order. Request the test report for the grade you require — such as accelerated weathering per ISO 4892 or equivalent — so you can confirm it meets your end-market labelling or compliance obligation before production begins.
Q: How does LDPE lamination compare to PVC knife coating at flex points?
A: LDPE lamination bonds a film layer onto the HDPE weave surface, while PVC knife coating penetrates into the yarn bundle. At repeated flex points, lamination may micro-crack along fold lines if the bond was insufficient. For applications involving constant folding — such as removable truck covers — specifying lamination weight per side and requesting a flex-durability sample helps validate long-term performance for PE Tarpaulin Roll material and coating in your application.
Q: How is colour consistency controlled across multiple rolls in one order?
A: Colour is matched to a reference standard at the compounding stage, and each production batch undergoes visual comparison under controlled lighting. Rolls from the same batch are grouped for dispatch to minimise variation. For large orders spanning multiple batches, request a colour tolerance sample set before shipment so you can approve the acceptable range for side-by-side installation.