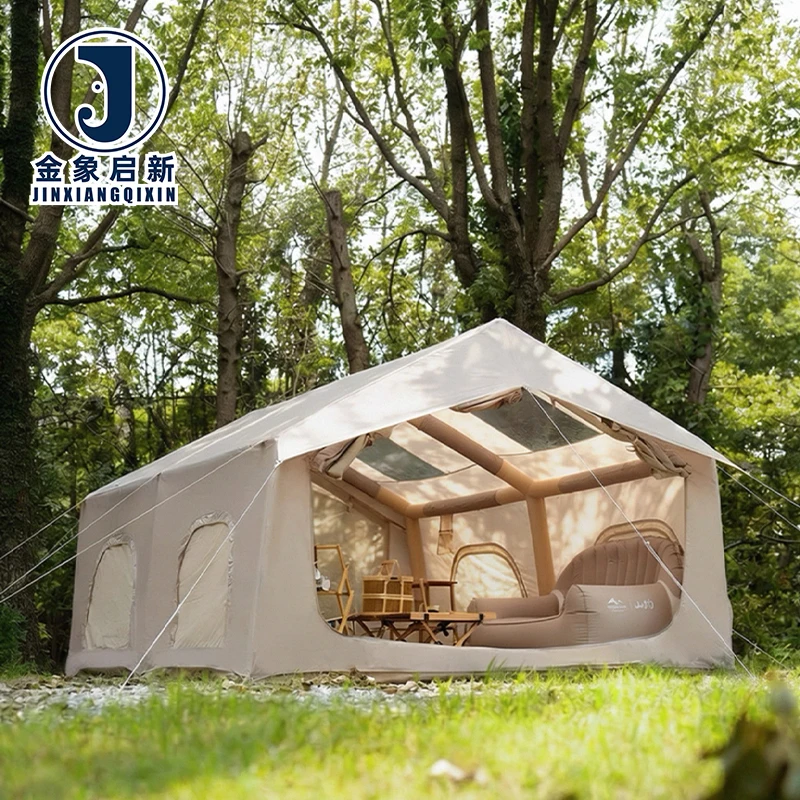
Process-Controlled Coating — Three full production lines maintain consistent PVC coating adhesion across every roll of inflatable tent fabric, verified through in-process quality checks before shipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent Fabric |
| Core Material | PVC waterproof fabric |
| Product Forms | Single Layer Construction, Extended Type |
| UV Treatment | UV resistant (test basis not stated in source — confirm test standard for your market) |
| Waterproof | Yes (waterproof rating not stated in source) |
| Flame Retardant | Available in flame retardant grades — confirm the grade required for your market |
| Season Rating | Four-season |
| Certifications | ISO9001, ISO14001, ISO45001, CE |
| Customization | OEM & ODM support, material selection, product design modifications, pattern printing |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Temporary site offices at construction projects | Continuous outdoor weathering, wind load on inflatable tubes, daily UV exposure |
| Equipment storage facilities during outdoor operations | Water ingress prevention, material handling abrasion at base and entry points |
| Mobile command centers for industrial events | Rapid deployment cycles, repeated inflation and deflation stress on seams |
| Emergency response shelters for infrastructure maintenance | All-season temperature fluctuation, portable transport and rough site handling |
| Disaster relief shelters | Immediate deployment under harsh conditions, multi-week continuous occupancy |
Why Unverified Material Claims Create Compliance Risk on Shelter Projects
Technical buyers need documented test results, not marketing statements, to approve PVC Inflatable Tent Fabric material for regulated sites.
When a shelter project specifies UV resistance or flame retardancy, the procurement team must present verifiable test documentation to the site safety officer or the local authority having jurisdiction. A claim without a referenced standard leaves the buyer exposed at the inspection stage [NEED_CITE: fire classification requirements for temporary structures per local building codes]. Inflatable tent fabric that fails to produce a batch-specific test report often results in rejected deliveries, re-procurement delays, and contractual penalties. This page outlines how PVC Inflatable Tent Fabric material is specified, tested, and documented so technical buyers can match the fabric to the exact compliance framework their project demands.
Coating Weight and Seam Integrity Under Inflation Pressure
Inflatable tent tubes operate under continuous internal pressure, placing sustained stress on every welded seam. The PVC coating must bond to the base fabric with sufficient adhesion strength to resist peeling at the heat-weld line. When PVC Inflatable Tent Fabric material is produced with controlled coating weight, the thermal profile during high-frequency or hot-air welding remains predictable, allowing fabricators to dial in consistent weld parameters. Inconsistent coating thickness leads to uneven melt behaviour, producing weak spots that reveal themselves only after the structure is inflated and under load.
Base Fabric Construction and Tube Rigidity
The denier of the base yarns and the weave density determine how much the inflatable tube resists deformation when wind loads or occupant contact apply lateral force. A tighter weave distributes point loads across more yarns, reducing the chance of localized tearing at stress concentrations. For single-layer construction tents, the base fabric carries the entire structural load without a secondary frame, making the selection of base fabric denier a primary design decision. Extended-type configurations add interior volume, increasing the surface area under tension and further elevating the importance of tensile and tear performance in the PVC Inflatable Tent Fabric material specification.
Interpreting the Specification Sheet for Inflatable Applications
GSM alone does not define how a coated fabric will behave in an inflatable structure. The relationship between base fabric denier, weave density, and coating weight collectively determines tensile strength, tear resistance, and weld performance [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421]. A heavier coating applied over a low-denier base fabric may achieve a high GSM figure while delivering lower tear propagation resistance than a lighter coating on a high-denier, tightly woven base. Knife-coated PVC achieves deeper penetration into the fabric interstices, producing higher peel strength at the weld line compared to laminated constructions. For inflatable tent tubes that undergo repeated pressurization cycles, peel strength directly governs whether the seam or the fabric body fails first. Surface finish — glossy or matte — affects both cleanability in field conditions and the adhesion of printed graphics or branding applied after fabrication. Flame retardant grades must be matched to the fire safety code enforced at the deployment site, as different jurisdictions reference different test standards.
The Hidden Cost of Specifying Without Verification
When the material specification sheet does not match the physical roll on arrival, the consequences extend beyond a single rejected shipment. Fabricators who have already cut and welded panels from an under-weight roll face scrap costs and schedule delays that cascade through the project timeline. Flame retardant grades that lack supporting test documentation can halt a shelter installation at the commissioning stage, forcing the contractor to source replacement material under emergency lead times [NEED_CITE: temporary shelter fire safety inspection protocols]. Colour variation between rolls in the same order becomes visible once panels are joined, requiring rework or acceptance of an inconsistent appearance across the finished structure. Weld failures that originate from inconsistent coating adhesion may not appear during factory quality checks but manifest after the inflatable tent is pressurized and exposed to temperature cycling on site.
Why Procurement Teams Source Inflatable Fabric Here
Three dedicated production lines allow bulk roll output for large shelter projects while maintaining coating consistency across the entire order. The ten-person R&D team develops custom material selections and sample prototypes within days, enabling fabricators to validate weld parameters and colour accuracy before committing to full production. Every production stage includes dedicated quality inspection, with one hundred percent pre-shipment review ensuring that the PVC Inflatable Tent Fabric material dispatched matches the agreed specification. ISO and CE certifications are maintained across the facility, providing the audit trail that regulated procurement environments require. Pattern printing and custom sizing are handled in-house, reducing the number of hand-offs between material supply and finished product delivery.
Documentation & Verification
- Material specification sheet stating GSM, base fabric denier, and coating weight per roll
- UV and flame retardant test reports referencing the exact standard and grade applicable to the batch
- ISO9001, ISO14001, ISO45001, and CE certificates available for buyer audit before order confirmation
- Pre-shipment inspection record with batch-specific coating adhesion and dimensional quality data
- Roll packing list with individual roll identification for traceability through fabrication
- Certificate of origin and customs documentation for international shipment clearance
Fabrication, Handling & Storage
- High-frequency welding parameters should be calibrated to the specific PVC coating weight before production runs begin
- Single-layer inflatable tube seams require overlap width matched to the base fabric denier for adequate peel strength
- Store rolls vertically on end caps to prevent flat-spot deformation of the PVC waterproof fabric surface
- Allow cold-stored rolls to reach ambient temperature before unrolling to avoid coating micro-cracking
- Use mild detergent solutions for field cleaning; solvent-based cleaners may degrade the PVC coating surface
- Repair minor punctures with compatible PVC adhesive patches applied to clean, dry fabric surfaces
What to Include in Your Inquiry
Provide the target deployment environment, including expected temperature range and UV exposure duration, so the appropriate treatment grade can be recommended. Specify the fire safety code or standard enforced at your project site to ensure the flame retardant grade aligns with local requirements. Indicate whether you require rolls for in-house fabrication or finished cut-to-size panels with welded seams and pattern printing.
Frequently Asked Questions
Q: How is UV resistance measured and what test basis supports the stated performance?
A: UV resistance testing follows recognized standards that expose coated fabric samples to controlled ultraviolet radiation over defined periods, measuring colour shift and tensile retention afterward. The specific test method and exposure duration vary by market requirement. Request the test report referencing the standard applicable to your deployment region before confirming your PVC Inflatable Tent Fabric material order.
Q: Which flame retardant grades are available for inflatable tent structures?
A: Flame retardant grades are produced to match different regional fire safety codes, and the correct grade depends on the jurisdiction where the shelter will be deployed. Available options should be confirmed against your project specification. Ask for the test report corresponding to the grade required by your local authority having jurisdiction before placing a production order.
Q: What base fabric denier and GSM options suit different inflatable tube diameters?
A: Larger tube diameters require higher tensile and tear performance to withstand the greater surface tension under inflation pressure. Base fabric denier and coating weight are selected together to achieve the necessary strength profile. Share your tube diameter and operating pressure so the PVC Inflatable Tent Fabric material specification can be matched to your structural design requirements.
Q: How does PVC coating weight affect weld strength on inflatable seams?
A: Coating weight influences the thermal energy required to achieve a proper weld and the resulting peel strength at the seam. Heavier coatings may require adjusted welding parameters to ensure full fusion without degrading the base fabric. Fabricators should run test welds on sample material from the production batch to confirm optimal settings before commencing full-scale tube fabrication.
Q: Can custom width and colour be produced with batch consistency documentation?
A: Custom widths and colours are produced on dedicated production lines with in-process quality controls monitoring coating weight and colour uniformity across every roll. Batch-specific inspection records document the measured values for each roll shipped. Confirm your width, colour reference, and annual volume requirements so production scheduling can ensure consistent output across your order history.