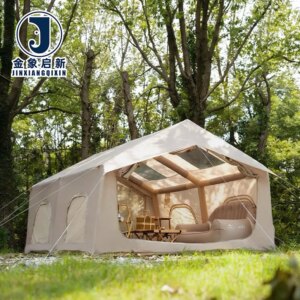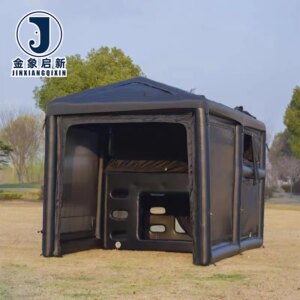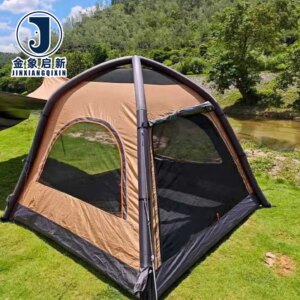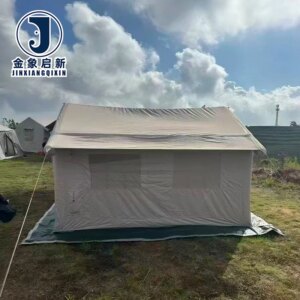
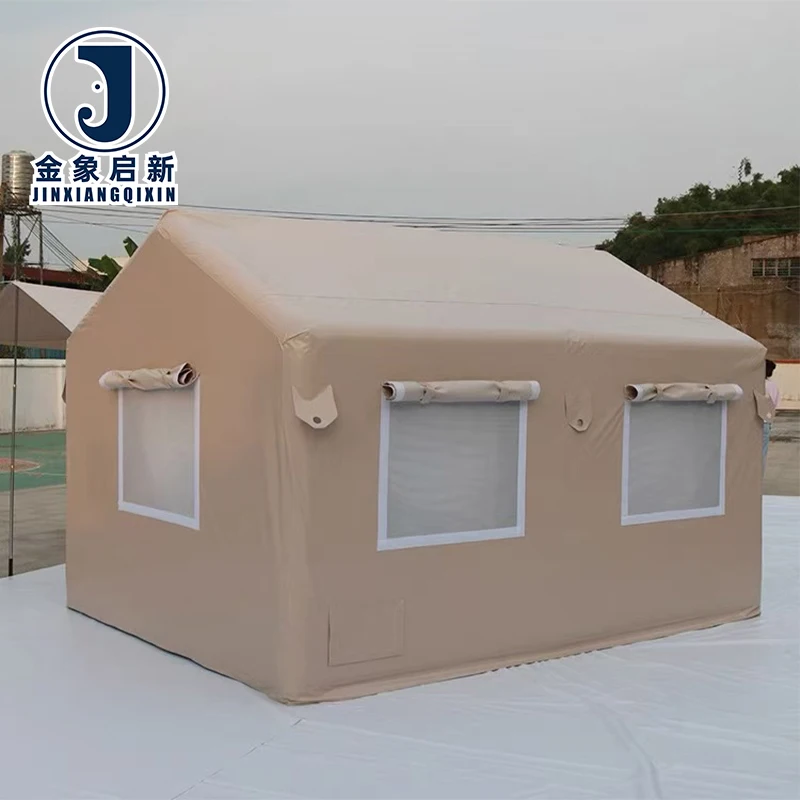
Coating Adhesion & Seam Integrity — Every roll of PVC inflatable shelter fabric undergoes stage-by-stage process control across 3 full production lines, ensuring coating weight consistency and reliable heat-weld performance where inflation pressure concentrates stress.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable tent |
| Core Material | PVC Tarpaulin |
| Key Performance | Waterproof, UV-resistant, Tear-resistant |
| Capacity | 6-8 persons |
| Deployment Feature | Quick Automatic Opening |
| Construction | Single Layer, Extended Type, Four-Season |
| Customization | OEM & ODM (material selection, design, pattern printing) |
| UV Resistance | Available in UV-resistant grades — confirm the test basis required for your market |
| Flame Retardant | Available in flame retardant grades — confirm the grade required for your market |
| Standards & Certification | ISO 9001, ISO 14001, ISO 45001, CE |
| Quality System | Full-process inspection with dedicated QA/QC staff |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Temporary site offices during infrastructure projects | Continuous UV exposure, wind-driven rain, daily inflation/deflation cycles requiring stable seam adhesion |
| Emergency response command centers for disaster recovery | Rapid deployment under adverse weather, need for reliable waterproof integrity and tear resistance at flex points |
| Equipment storage in remote construction areas | Long-term static load, dust and moisture ingress prevention, abrasion from stored machinery |
| Temporary warehousing for logistics hubs | Four-season thermal variation, repeated structural tensioning, forklift proximity abrasion risk |
What Happens When Coating Fails Before the Base Fabric Does
Seam separation under inflation pressure is a coating formulation and welding parameter problem, not a base fabric thickness problem.
Technical buyers reviewing PVC inflatable shelter fabric often focus on base fabric denier and overall weight. Yet in practice, a significant proportion of field failures in inflatable membrane structures originate at the heat-welded joints. The coating layer must transfer load evenly into the base fabric at these junctions. When adhesion is insufficient or the welding temperature window is too narrow, the seam becomes the weakest link [NEED_CITE: peel adhesion test methods for coated fabrics per ISO 2411]. Specifying coating weight and adhesion values — not just total GSM — prevents this mismatch.
Coating Weight and Formulation for Airtight Membrane Performance
The PVC coating on inflatable shelter fabric serves two simultaneous functions: it creates the airtight barrier that holds inflation pressure, and it provides the surface that bonds during heat welding. Coating weight directly influences both. A heavier coating layer generally improves airtightness but requires precise temperature control during welding to avoid burning through the surface before achieving full bond depth. Buyers should request the coating weight specification separately from the base fabric weight to understand how the total PVC inflatable shelter fabric construction balances these requirements.
Heat Welding Compatibility and Seam Strength at Stress Points
Inflatable structures concentrate mechanical stress at curved junctions and connection ports. Heat-welded seams in these zones must match or exceed the tensile strength of the parent PVC inflatable shelter fabric. The welding process melts the coating layers of two fabric panels together, creating a molecular bond. Consistent coating formulation across the roll width ensures uniform melting behaviour, preventing cold spots where bond strength drops. Production facilities with in-line coating weight monitoring maintain this consistency across large batches.
Base Fabric Denier and Weave Density Under Tension
The base fabric provides the structural skeleton that resists inflation pressure without stretching beyond design limits. Higher denier yarns and tighter weave patterns increase both tensile and tear strength. For inflatable shelters that experience dynamic wind loads, the weft yarns must resist propagation of any puncture into a full tear. Specifying both denier count and mesh density — rather than relying on total weight alone — gives a clearer picture of how the PVC inflatable shelter fabric will behave under sustained inflation pressure [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421].
UV Treatment Longevity for Extended Outdoor Deployment
Inflatable shelters deployed in open environments receive uninterrupted solar radiation. UV stabiliser packages within the PVC coating slow the embrittlement process that causes surface cracking and colour fade. The effectiveness of these additives depends on both the type and the concentration used. Buyers sourcing for projects in high-UV regions should request the specific UV test report to verify that the treatment level matches the expected service exposure, rather than relying on a generic "UV-resistant" label.
The Hidden Cost of Specifying on Weight Alone
Procurement teams that select coated fabric based solely on total GSM often discover after delivery that the material behaves differently from the sample they approved. A heavier coating with a lighter base fabric may pass the weight check but deliver lower tear strength than expected. Conversely, a balanced construction at the same total weight can outperform it significantly. Batch-to-batch colour variation also compounds the problem when panels from different rolls are welded side by side on an inflatable structure, making inconsistencies visible across the entire surface [NEED_CITE: colour fastness evaluation methods for coated textiles]. Requesting the full material breakdown — base fabric weight, coating weight, denier, and weave count — prevents these mismatches.
Why Source PVC Inflatable Shelter Fabric Through This Facility
- Deep coating process control: Nearly 30 years focused on coated fabric production delivers repeatable coating adhesion and weight accuracy across all inflatable shelter rolls.
- Dedicated R&D support: A 10-person technical team handles material selection, custom formulation, and sample development, producing test panels within days for buyer evaluation.
- Full in-house capacity: 3 production lines and 36 sets of professional equipment support bulk orders with maintained lead-time reliability for time-sensitive emergency shelter projects.
- Stage-gated quality assurance: 100% inspection before shipment, with dedicated QA/QC personnel verifying coating weight, seam peel strength, and colour consistency on every roll.
Documentation & Verification
- Material specification sheet detailing GSM breakdown into base fabric and coating weight per roll
- UV and flame-retardant test reports issued against recognised standards where applicable
- ISO 9001, ISO 14001, ISO 45001, and CE certificate copies for compliance filing
- Pre-shipment inspection record confirming coating weight, colour match, and seam test results
- Roll packing list with batch numbers traceable to production date and line
Fabrication, Handling & Storage
- Set heat-welding temperature based on the specific PVC coating formulation to prevent surface scorch or incomplete bonding at seam edges.
- Store rolls horizontally on padded racks to avoid compression marks on the PVC coating surface that may affect airtightness.
- Unroll fabric in temperatures above 5 °C to prevent micro-cracking in the PVC coating layer during handling.
- Use PVC-compatible solvent cleaners on the coated surface; avoid hydrocarbon-based products that soften the coating and weaken seam bonds.
- Plan cutting layouts to minimise offcuts and reduce the number of welded seams in high-stress inflation zones.
- Repair field punctures with matching PVC inflatable shelter fabric patches, heat-welded to maintain airtight continuity.
Project Specification and Enquiry Guidance
When requesting a quotation for PVC inflatable shelter fabric, include the deployment environment — climate zone, expected wind load category, and average UV index — so the correct coating formulation and UV stabiliser package can be recommended. Specify whether you require raw roll stock for your own fabrication or finished cut-and-welded panels to a pattern you provide. If your destination market mandates a particular flame-retardant classification, state the exact standard and grade so the appropriate test report can be prepared in advance. Sample rolls are available for internal weld testing before full order commitment.
Frequently Asked Questions
Q: What GSM and coating weight breakdown is recommended for airtight inflatable structures?
A: Total GSM alone does not confirm airtightness. The coating weight as a percentage of total weight matters more. Request the full specification sheet showing base fabric weight and coating weight separately. Our technical team can recommend a formulation based on your inflation pressure and operating temperature range.
Q: How does heat welding affect seam strength compared to stitching?
A: Heat welding fuses the PVC coating layers into a continuous bond, eliminating needle holes that compromise airtightness. Welded seams can match or exceed the parent fabric strength when coating formulation and welding parameters are correctly aligned. Stitching introduces perforations that require additional sealing in inflatable applications.
Q: What UV treatment options extend outdoor service life?
A: UV stabiliser packages are added during the coating compounding stage. The concentration and type determine long-term resistance to embrittlement and colour fade. We supply UV test reports for applicable grades so you can verify the treatment level matches your deployment environment before committing to bulk production.
Q: Can custom dimensions and colours be produced with batch consistency?
A: Yes. Our 3 production lines and in-house coating facilities allow colour matching and custom widths across large volumes. Each roll is checked against the approved colour standard during pre-shipment inspection to prevent visible variation when panels from different rolls are welded together on site.
Q: What quality documentation accompanies each shipment?
A: Every dispatch includes a material specification sheet with the GSM breakdown, a pre-shipment inspection record, roll packing list with batch traceability, and relevant ISO and CE certificates. UV and flame-retardant test reports are provided where the specified grade requires them.