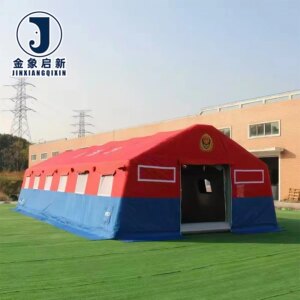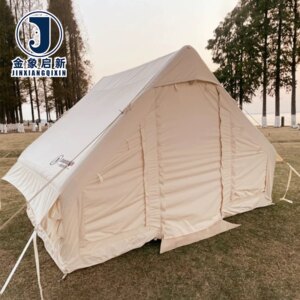
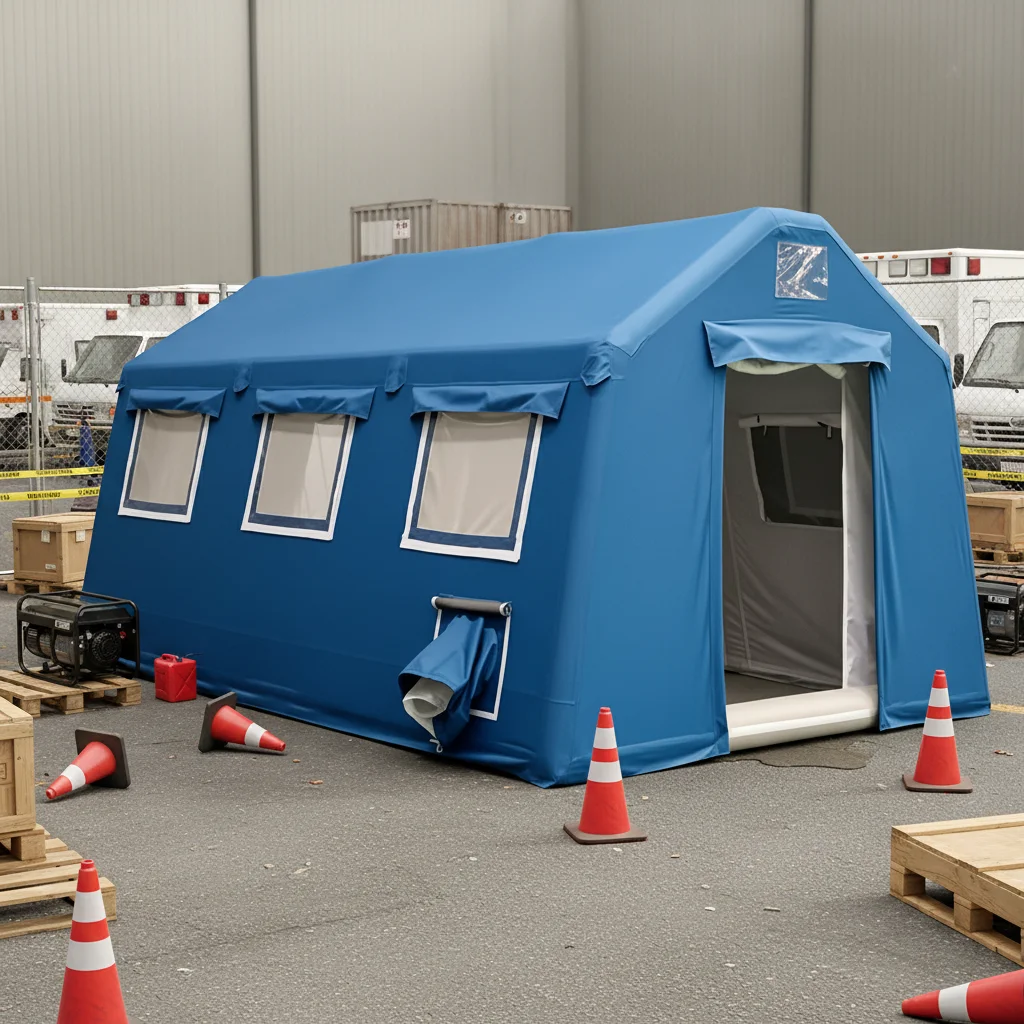
Deep Coating Process Control — verified at every production stage with batch-level adhesion and weight checks, ensuring inflatable structures hold pressure under field conditions.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent |
| Core Material | PVC tarpaulin (PVC knife-coated fabric) |
| Construction | Single layer |
| Deployment Type | Quick automatic opening |
| Tent Form | Extended type |
| Season Rating | Four-season |
| Waterproof | Yes — fully waterproof coated construction |
| UV Treatment | UV-resistant (grade not stated — confirm test basis for your market) |
| Flame Retardant | Fire-retardant properties available (grade not stated — confirm the grade required for your market) |
| Tear Resistance | High tear resistance (test standard not stated) |
| Tensile Strength | Exceptional tensile strength (test standard not stated) |
| Seam Technology | Waterproof seam, welded |
| Air Pressure Retention Test | Minimum 24 hours per unit |
| Quality Inspection | 100% pre-shipment, on-site QA&QC at every stage |
| Customization | OEM & ODM, size adjustments, color options, pattern printing, specialized access configurations |
| Standards | ISO9001, ISO14001, ISO45001, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Emergency disaster relief shelters | Rapid deployment under severe weather, wind load, repeated inflation and deflation cycles |
| Emergency response command centers | Extended occupancy, climate exposure, internal equipment protection from water ingress |
| Temporary storage during disaster recovery | Moisture and debris protection, structural stability over uneven ground |
| Mobile field operations bases | Multi-season outdoor exposure, UV radiation, mechanical stress from setup and teardown |
| Infrastructure maintenance project shelters | Year-round weather resistance, fire safety compliance on regulated sites |
Why "Flame Retardant" Means Nothing Without a Test Report Behind It
Specifying PVC inflatable tent fabric without documented fire classification creates a compliance gap that only surfaces at the point of site inspection or after an incident.
Most inflatable shelter failures tied to fire safety trace back not to the fabric itself failing but to a missing or generic certificate that does not match the jurisdiction’s accepted test method. A material described as fire-retardant without naming the standard leaves the buyer exposed when the project safety officer asks for proof. [NEED_CITE: fire classification standards for temporary structures vary by region and enforcing authority]
I have seen procurement teams accept a supplier’s self-declaration only to discover the test was run on a different base fabric or an outdated coating formulation. The consequence is not just paperwork — it is a shelter that cannot legally be occupied until a compliant material is sourced and fabricated under pressure. This is why every batch of our knife-coated PVC inflatable shelter material ships with documentation that ties the fire performance claim to a specific standard and production run.
How Knife-Coated Construction Delivers Structural Integrity Under Inflation Pressure
The knife-coating process forces PVC compound into the interstices of the base fabric rather than simply bonding a film to the surface. This penetration creates a mechanical lock between coating and yarn that resists delamination during the repeated stress cycles an inflatable structure endures. When air beams flex under wind gusts or snow load, the coating stays bonded where laminated alternatives begin to separate at the edges.
For technical buyers specifying PVC inflatable tent fabric for rapid-deployment shelters, this coating method directly affects how many inflation cycles the structure can tolerate before seam stress becomes visible. The deeper the coating penetration, the more uniformly the load transfers across the fabric surface rather than concentrating at weld points.
Waterproof Seam Technology and Why Welded Joints Are the First Point of Failure
Every inflatable shelter relies on seams that must hold both air pressure and external loads simultaneously. Welded seams on knife-coated PVC tarpaulin fuse the coating layers into a continuous bond, eliminating the needle holes and thread degradation that compromise stitched alternatives. When the shelter flexes at the junction between air beam and canopy panel, the weld must stretch at the same rate as the parent material. [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421]
A seam that is stiffer or more brittle than the surrounding fabric will crack under thermal cycling or repeated inflation. Our waterproof seam process is tuned to the specific coating formulation of our PVC knife-coated fabric, so the weld zone matches the flexibility of the body material through seasonal temperature swings.
Reading Between the Lines on Coated Fabric Specifications
GSM alone tells you the weight of material per square meter but says nothing about how that weight is distributed between base fabric and coating. A heavy coating on a loosely woven base may meet the target GSM while delivering poor tear resistance because the yarn structure cannot arrest a tear once initiated. Conversely, a tightly woven base with a thinner, well-penetrated knife coat can outperform a heavier alternative in both tensile and tear tests. For inflatable structures, the base fabric denier and weave density determine how well the air beams resist deformation under internal pressure while the coating provides the airtight barrier and environmental protection. The relationship between these two elements — not the combined weight — is what governs real-world performance. Coating adhesion strength, measured as peel resistance between layers, becomes critical at welded seams where the heat-affected zone can weaken the bond if the formulation is not matched to the welding temperature window.
What Happens When Material Specification Is Based on Marketing Claims Instead of Test Data
When anti-UV treatment is declared without a test basis, the first visible sign of failure is surface chalking and embrittlement after a single season of full sun exposure. For inflatable shelters deployed in disaster zones where replacement logistics are difficult, this means the structure becomes unreliable precisely when it is needed most. Flame-retardant claims without a named grade lead to site rejection, project delays, and potential liability exposure for the deployment organization. [NEED_CITE: accelerated weathering test protocols for coated fabrics used in temporary structures]
Batch-to-batch variation in coating weight compounds these problems when rolls from the same purchase order perform differently in the field. Fabricators who cut and weld multiple rolls into a single shelter may find that some panels hold air pressure while adjacent panels show early creep at the seams.
Why Technical Buyers Source Knife-Coated PVC Here
Deep process control over coating weight and adhesion is maintained across three full production lines with 36 sets of professional equipment, giving consistent output from the first roll to the last in a production run.
A 10-technician R&D team handles material selection, custom sizing, and sample development specific to inflatable structure requirements, shortening the path from specification to approved sample.
Dedicated QA and QC personnel inspect at every production stage, with a mandatory 24-hour air pressure retention test on every inflatable unit before dispatch — not a spot-check on a random sample.
Full documentation traceability ties each roll back to its coating batch, base fabric lot, and inspection record, so material performance can be verified independently.
ISO9001, ISO14001, ISO45001, and CE certifications are maintained as operating standards rather than display items, with audit records available for buyer review.
Documentation & Verification
- Material specification sheet stating base fabric, PVC coating method, and performance parameters per production batch
- Test reports for UV resistance and flame-retardant grades confirming the specific standard applicable to your market
- ISO and CE certificates linked to the production facility and batch inspection records
- 24-hour air pressure retention test log and seam tensile evaluation per unit before dispatch
- Certificate of origin and customs documentation prepared per shipment destination
Fabrication, Handling & Storage
- Set hot-air welder temperature to match PVC knife-coated fabric formulation — incorrect heat causes delamination at seam edges
- Store rolls horizontally on padded racks to prevent permanent creasing that weakens the coating at fold lines
- Allow cold-stored PVC tarpaulin rolls to acclimatize before unrolling to avoid coating crack at low temperatures
- Use compatible PVC-based repair adhesive matching the knife-coated surface chemistry for field patches
- Plan cutting layout to minimize cross-grain seams on air beam panels where inflation pressure concentrates stress
Specifying Your PVC Inflatable Shelter Project
Provide the deployment environment — climate zone, expected wind exposure, and duration of continuous inflation — so the correct base fabric and coating weight can be recommended. State the fire safety standard required by the jurisdiction where the shelter will be erected, as flame-retardant grades differ by market. Indicate whether you need raw rolls for your own fabrication line or finished units with custom access configurations and pattern printing.
Frequently Asked Questions
Q: What coating method is used and how does it affect tensile and tear strength for inflatable structures?
A: We use knife-coated PVC construction where the compound is driven into the base fabric interstices rather than laminated as a surface film. This creates a mechanical bond between coating and yarn that resists delamination under the repeated inflation and deflation cycles an inflatable shelter experiences. The deeper penetration distributes load across the fabric surface more uniformly, reducing stress concentration at welded seams and improving overall tear propagation resistance.
Q: What flame-retardant grade is available and does it meet my target market’s fire safety requirements?
A: Fire-retardant PVC formulations are available, but the specific grade must be confirmed against the fire classification standard enforced in your deployment region. Different jurisdictions accept different test methods — some require DIN 4102 classification, others reference NFPA or local building codes. Provide your target market and applicable standard so we can supply the correct formulation with supporting test documentation tied to your production batch.
Q: What is the UV-resistance test basis and expected performance under prolonged outdoor exposure?
A: UV-resistant additives are compounded into the PVC coating to reduce degradation from continuous sun exposure during extended field deployment. The specific test basis and exposure duration should be confirmed against your project’s expected service conditions. We recommend requesting the UV test report matched to your batch so you can evaluate the data against your own performance requirements and regional climate intensity.
Q: How are welded seams tested for integrity under inflation pressure and flex cycling?
A: Every inflatable unit undergoes a minimum 24-hour air pressure retention test before shipment, verifying that all welded seams hold under continuous inflation. Seam tensile strength is evaluated through standardized testing to confirm the weld zone matches the flexibility of the parent PVC knife-coated fabric. This catches seam failures that would otherwise appear only after repeated setup and teardown cycles in the field.
Q: Can you supply raw material certificates and coating weight documentation for regulatory compliance?
A: Yes. Each shipment includes a material specification sheet stating the base fabric construction, PVC coating method, and weight parameters per production batch. ISO9001, ISO14001, ISO45001, and CE certificates are provided alongside batch inspection records. For projects requiring regulatory submission, we supply documentation that traces the fabric back to its coating batch and base fabric lot for independent verification.