Proven coating adhesion — Nearly 30 years of process control over knife coating weight and base fabric bonding, validated through 100% pre-shipment inspection on every roll.
Technical Specifications
| Parameter | Value |
|---|---|
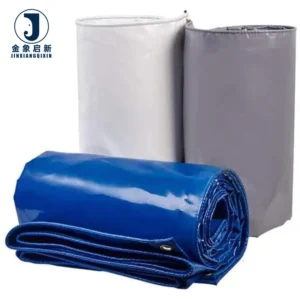
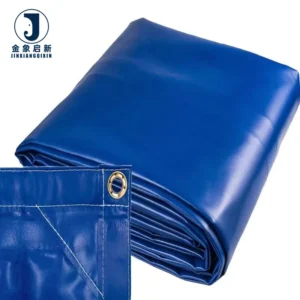
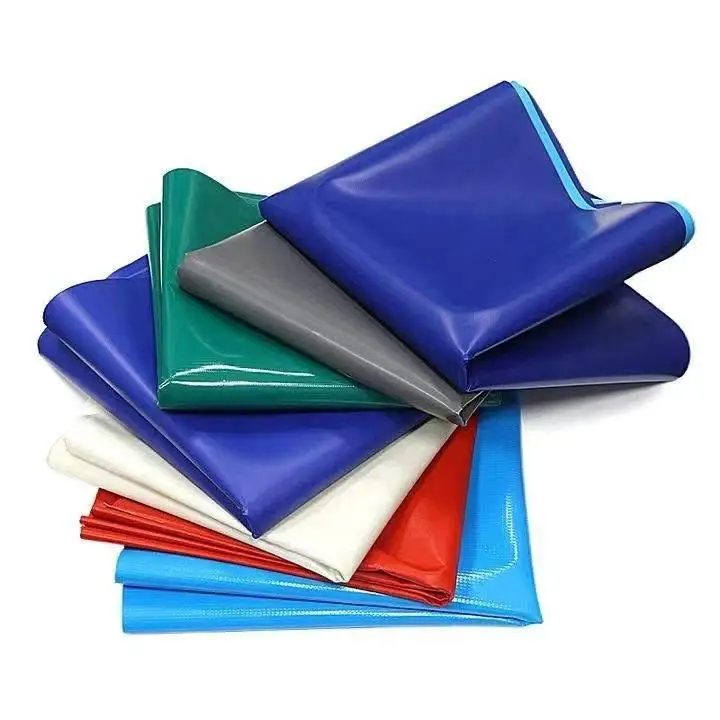
| Product Type | Blue PVC Knife Coated Tarpaulin Heavy Duty Waterproof Truck Cover Fabric |
| Material | PVC Knife Coated Fabric |
| Coating Method | Knife over roll |
| Coating Material | PVC (Polyvinyl Chloride) |
| Surface Finish | Self-cleaning top coat |
| Flame Retardant | Available in flame retardant grades — confirm the grade required for your market |
| UV Treatment | UV resistant formulation available — test basis to be confirmed per specification |
| Antibacterial | Yes |
| Anti-Mildew | Yes |
| Oil & Stain Resistance | Yes |
| Acid & Alkali Resistance | Yes |
| Temperature Performance | High temperature and cold resistant (range to be confirmed) |
| Oxidation Resistance | Yes |
| Weather Resistance | Yes |
| Flexibility | Highly flexible, crack resistant |
| Welding Compatibility | HF (High Frequency), Hot Air, Sewing |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Tensile and membrane structures | Sustained tension loads, wind uplift, UV and thermal cycling — demands consistent coating weight and high peel strength at seams |
| Airport hangars and portable storage | Extended weathering, large unsupported spans, fire safety compliance — requires verified flame retardant grade and dimensional stability |
| Stadium architectural fabrics | Long-term UV exposure, public safety fire codes, complex curvature — needs confirmed UV test basis and certified fire classification |
| Shade systems and large format textiles | Direct solar exposure, mechanical fastening points, surface cleanliness — benefits from self-cleaning finish and crack resistance |
| Truck covers and transport fabric | Constant flexing at load points, road abrasion, weather exposure — demands strong seam integrity and flex-point durability |
Why Coating Weight Claims Without GSM Verification Cost You at the Loading Bay
A stated GSM on the quotation means nothing if the roll arriving at your facility has not been independently weighed and recorded.
Technical buyers reviewing knife coated PVC tarpaulin fabric often encounter a gap between the specification sheet and the material on the cutting table. A roll that arrives lighter than agreed will show reduced tensile capacity, weaker tear resistance, and thinner coating layers that compromise both weld strength and weather performance [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421]. When the base fabric denier or weave density is lower than specified, the entire performance envelope shifts downward — and the failure typically appears at the weld line or the eyelet reinforcement point, not in the body of the fabric.
The verification step that prevents this is straightforward: demand a roll-by-roll GSM check documented in the pre-shipment inspection record, matched against the material specification sheet that accompanied the quotation. Without that paper trail, you are accepting material on trust alone.
Knife Coating Method and Peel Strength Advantage
The knife over roll coating process forces PVC paste directly into the base fabric weave under controlled pressure, creating a mechanical bond that substantially outperforms laminated or calendered alternatives in peel resistance. For knife coated PVC tarpaulin fabric used in tensile structures and truck covers, this adhesion quality determines whether the coating delaminates under cyclic loading or remains bonded through years of flex and tension. The coating weight per side can be precisely controlled during production, giving technical buyers a reliable specification to verify against incoming material.
Welding Compatibility and Seam Integrity
This material supports high frequency welding, hot air welding, and conventional sewing — each producing different seam characteristics suited to different fabrication requirements. HF welding creates a molecular bond between PVC layers that can match or exceed the base fabric strength, making it the preferred method for membrane structures and pressurised duct applications. Hot air welding offers greater flexibility for on-site repairs and complex geometry, while sewn seams with taped overlays suit applications where mechanical fastening is also present [NEED_CITE: weld strength testing methods for coated technical textiles]. The choice of welding method should align with the stress profile of the finished product.
How Base Fabric Construction Drives Real-World Performance
The tensile and tear behaviour of any PVC coated fabric is governed by the interaction between base fabric denier, weave density, and total coating weight — not by GSM alone. A heavier GSM achieved through excess coating on a light base fabric will feel substantial but tear more easily than a balanced construction with moderate coating on a high-denier, tightly woven substrate. The knife coating process allows the PVC to penetrate the weave fully rather than sitting on the surface, which improves both the load transfer between yarns and the resistance to tear propagation. When specifying material for structural or transport applications, request the base fabric denier and weave count alongside the total GSM to understand how the fabric will behave under directional loads.
The self-cleaning surface finish reduces particulate adhesion and biological growth, which matters for architectural fabrics where maintenance access is limited and surface contamination accelerates UV degradation. The antibacterial and anti-mildew treatments further protect the coating interface in humid or marine-adjacent installations where biological attack on the PVC plasticiser can lead to embrittlement.
What Happens When the Weld Fails Before the Fabric Does
The most common point of failure in fabricated PVC covers and structures is the welded seam, not the body of the material. When coating weight is inconsistent across a roll, or when the base fabric weave varies in density, the weld parameters that worked on the sample piece may not transfer to production — resulting in seams that separate under load while the surrounding fabric remains intact [NEED_CITE: seam failure analysis in coated fabric fabrication]. This failure mode is particularly costly in truck cover applications where a split seam at a flex point exposes the load, and in tensile structures where seam failure under wind load creates immediate safety concerns. Consistent coating adhesion from the knife coating process reduces this risk, but weld procedure qualification on each production batch remains essential.
Why Procurement Teams Specify This Material from Jinan Jinxiang
Deep process control over coating weight and base fabric adhesion, developed through nearly 30 years of focused PVC coated fabric production, means the GSM on the specification sheet matches the roll on the cutting table. Three full production lines and 36 sets of professional equipment support bulk roll volumes with maintained consistency across the production run. A 10-person R&D team handles material selection, custom width and colour development, and sample preparation within days for project-specific requirements. Dedicated quality control at every production stage includes in-process coating weight checks and 100% pre-shipment inspection with roll-by-roll verification. All production operates under ISO and CE certified quality systems, with full documentation packages prepared for cross-border shipment and project approval submissions.
Documentation & Verification
- Material specification sheet stating total GSM, base fabric denier and weave, and coating weight per side
- Third-party test report for UV and flame retardant grades — request the specific standard reference applicable to your market
- Pre-shipment inspection record with roll-by-roll weight verification against the quoted specification
- ISO and CE certificates with certificate of origin for customs clearance and project compliance files
Fabrication, Handling & Storage
- Set HF welder dwell time and pressure based on the knife coated PVC thickness — trial welds on each new roll batch are essential before production
- Store rolls upright on end caps in a covered, ventilated area to prevent flat-spot deformation of the PVC coating surface
- Avoid dragging rolls across unprotected surfaces to prevent abrasion damage to the self-cleaning top coat finish
- Use compatible PVC-based repair adhesives and patches for field repairs, matching the knife coating formulation for bond strength
- Allow cold-stored rolls to reach ambient temperature before unrolling to prevent cracking of the PVC layer at low temperatures
Project Specification and Sampling Process
To move from enquiry to confirmed specification, provide the intended application and exposure conditions, the fire classification or UV test standard required in your target market, and the roll width and volume you need for the project. If you are fabricating finished products rather than buying standard rolls, share the cut sizes and welding method you use so we can align the material specification to your production process. Sample rolls are developed within days for custom requirements and can be tested in your own fabrication setup before bulk commitment.
Frequently Asked Questions
Q: How does knife coated PVC differ from laminated or calendered PVC in peel strength?
A: Knife coating forces PVC paste into the base fabric weave under pressure, creating a mechanical bond that delivers substantially higher peel resistance than laminated alternatives. This matters for tensile structures and truck covers where cyclic loading can cause coating delamination on lighter-bonded materials. Request a peel strength test result to compare directly.
Q: What flame retardant standard applies to my market and how do I verify it?
A: Fire classification requirements vary by region and application — building membrane structures, transport covers, and temporary structures each have distinct standards. Ask your local authority for the applicable classification, then request a test report referencing that specific standard. Generic flame retardant claims without a cited test method are insufficient for project approval.
Q: Can UV treatment and flame retardant treatment be combined in one fabric?
A: Both treatments can be incorporated into the PVC coating formulation simultaneously, but each requires its own independent test report to confirm performance. Verify that the UV test basis and the flame retardant grade are both documented and that neither treatment has compromised the other — request test results covering both properties on the same material batch.
Q: Which welding method gives the strongest seam for structural applications?
A: High frequency welding typically produces the highest seam strength by creating a molecular bond between PVC layers, making it preferred for tensile and membrane structures. Hot air welding offers flexibility for complex shapes and on-site work. The optimal choice depends on your fabrication equipment and the stress profile of the finished product — trial welds on sample material are recommended.
Q: How do you ensure roll-to-roll consistency across a bulk order?
A: Every production run undergoes in-process coating weight monitoring, and 100% pre-shipment inspection includes roll-by-roll GSM verification against the quoted specification. Colour consistency is checked across all rolls in the same order. The inspection record and material specification sheet are supplied with the shipment so you can verify compliance on receipt.