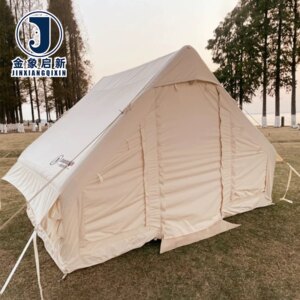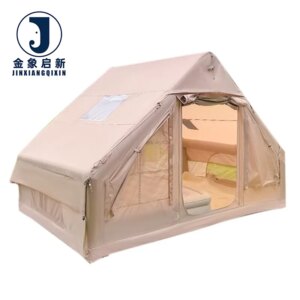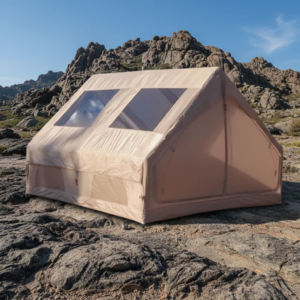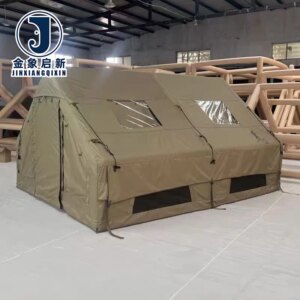
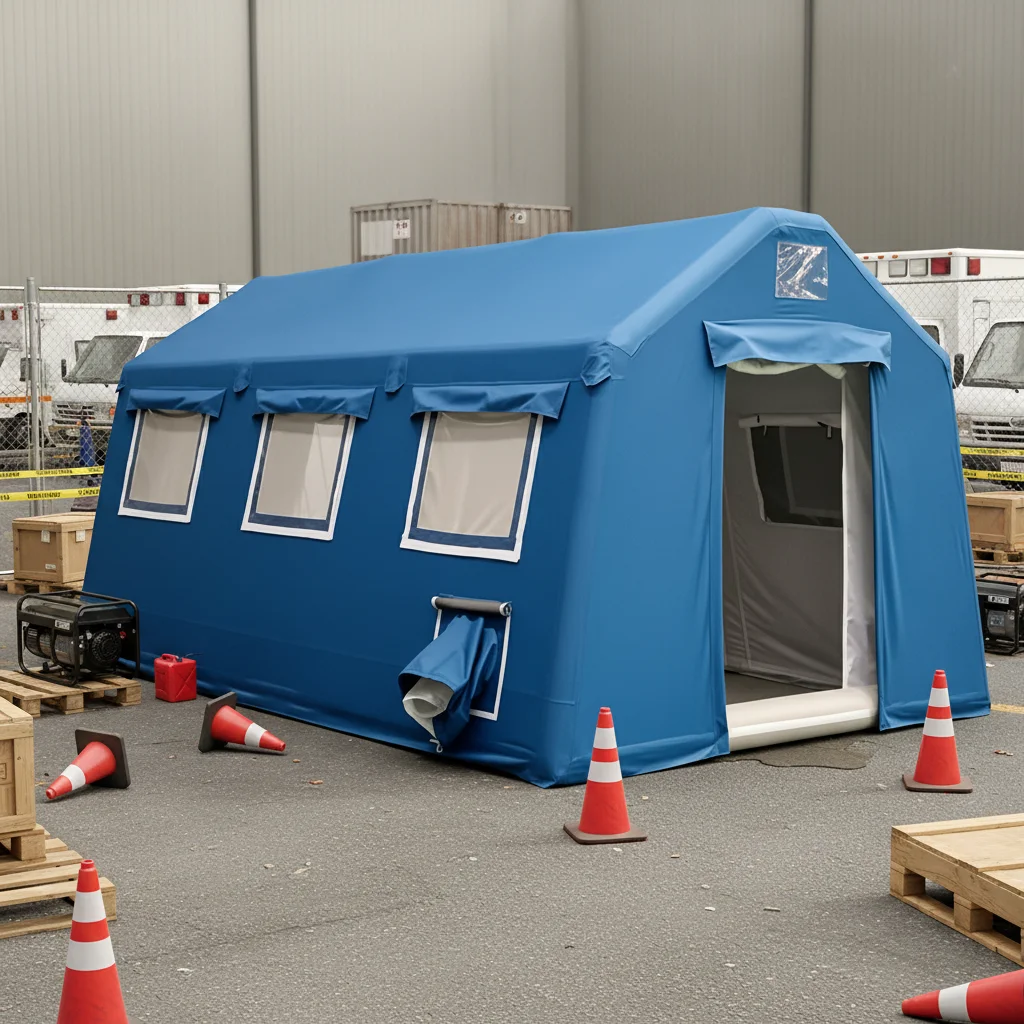
Process Control Over Coating Adhesion — Knife-coated PVC fabric produced on dedicated lines with in-process adhesion verification, ensuring consistent peel strength critical to airtight inflatable structures.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent |
| Core Material | PVC tarpaulin (knife-coated fabric) |
| Key Performance | Waterproof, tear-resistant |
| Flame Retardant | Fire-retardant properties claimed (grade not stated — confirm the grade required for your market) |
| UV Resistance | UV-resistant (test basis not stated — request test report for deployment duration validation) |
| Construction | Single layer, quick automatic opening, extended type |
| Customization | OEM & ODM, sample customization, pattern printing, size adjustments, color options |
| Standards | ISO9001, ISO14001, ISO45001, CE |
| Quality Control | 24-hour minimum air pressure retention testing, seam tensile testing, 100% pre-shipment inspection |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Emergency response command centers | Rapid inflation cycles, frequent redeployment, sustained air pressure retention across seams |
| Temporary storage during disaster recovery | Prolonged weather exposure, water ingress prevention, structural stability under wind load |
| Mobile field operations bases | Repeated setup and teardown, abrasion at ground contact points, UV exposure over extended periods |
| Infrastructure maintenance shelters | Four-season outdoor deployment, temperature cycling, wind-loaded membrane stress |
When "Fire-Retardant" PVC Lacks the Grade Your Site Inspector Requires
A fire-retardant claim without a documented grade is a compliance gap waiting to be discovered at the final inspection.
Technical buyers sourcing PVC inflatable tent fabric for emergency shelters and temporary structures frequently encounter supplier declarations that stop at "fire-retardant" without specifying whether the material meets B1, M2, NFPA 701, or the local building code classification. The consequence is not merely paperwork — it is a failed site acceptance that halts deployment and forces material replacement under compressed timelines. [NEED_CITE: fire classification standards for temporary structures and inflatable shelters] Fabric intended for disaster relief or industrial temporary shelters must carry a test report mapped to the standard enforced in the destination market, not just a generic assurance.
Coating Adhesion and Airtight Integrity in Inflatable Systems
The primary failure mode in inflatable tent structures is not the fabric tearing — it is the coating delaminating from the base fabric at the seam, allowing air to escape and the structure to lose rigidity. PVC inflatable tent fabric produced through knife-coating achieves a mechanical bond between the PVC compound and the woven polyester base that substantially exceeds the peel strength typical of laminated alternatives. This adhesion quality directly determines whether the inflated chamber holds pressure through temperature fluctuations and wind-loading cycles over repeated deployments.
Seam Engineering for Pressurized Membrane Structures
Every welded seam on an inflatable tent operates under constant internal pressure, meaning the joint must match or exceed the tensile performance of the parent fabric. The knife-coated surface provides a consistent PVC layer for hot-air or high-frequency welding, producing a homogeneous bond rather than a mechanical stitch that creates puncture points. Custom inflatable shelter material specified for rapid deployment shelters must be evaluated not only on base fabric denier but on the coating weight uniformity that enables predictable welding parameters across production batches. [NEED_CITE: weld strength testing methods for coated fabrics per ISO 1421]
Reading Beyond the Specification Sheet
Knife-coated PVC fabric construction delivers tensile and tear performance that depends on the interplay between base fabric weave density and total coating weight. A lighter base fabric with higher coating weight may inflate easily but resist abrasion poorly at ground contact points, while a heavier denier base with minimal coating provides structural rigidity at the cost of air permeability through micro-pores. The single-layer construction of this PVC inflatable tent fabric requires the coating to simultaneously provide waterproofing, UV protection, and the surface chemistry needed for reliable thermal welding — a balance that demands documented coating formulation control rather than generic material claims. Available in flame retardant grades — confirm the grade required for your market before placing production orders.
The Cost of Specifying Coating Weight Without Testing Weld Performance
A PVC coated fabric that tests well in isolation can still fail at the seam when thermal welding parameters are not matched to its specific coating formulation and thickness. Buyers who specify custom inflatable shelter material based solely on GSM and tensile data, without conducting weld trials on the actual production batch, risk discovering seam failure during the air pressure retention test — after the shelter has been cut, assembled, and is expected to hold pressure for deployment. [NEED_CITE: seam failure rates in inflatable structures under cyclic pressure loading] The financial impact extends beyond material waste to missed project deadlines and emergency procurement at premium lead times.
Why This PVC Coated Fabric Source Supports Technical Buyers
Three dedicated production lines allow parallel processing of different coating formulations, preventing cross-contamination between standard and flame-retardant PVC batches. A ten-technician R&D team develops custom samples within days, enabling weld parameter validation before bulk commitment. In-process quality checks at every coating stage catch adhesion and weight deviations before the fabric reaches the slitting line. Environmental simulation testing, including temperature cycling and UV exposure, is conducted on finished inflatable tent panels rather than raw roll stock alone. Each batch ships with air pressure retention test results from a minimum 24-hour hold, verifying that the material and its seams perform as a complete airtight system.
Documentation & Verification
- Material specification sheet detailing base fabric construction, coating method, and weight parameters for each production batch
- Test reports for UV resistance and flame-retardant grades where applicable, mapped to recognized testing standards
- ISO9001, ISO14001, ISO45001, and CE certificates available for project compliance packages
- Pre-shipment inspection records including air pressure retention test data and seam tensile evaluation
- Environmental simulation results covering temperature cycling and UV exposure for the specific batch produced
Fabrication, Handling & Storage
- Calibrate hot-air welding temperature and speed to the specific knife-coated PVC formulation before production runs begin
- Verify air pressure retention on welded test panels for a minimum of 24 hours before cutting full shelter components
- Store PVC inflatable tent fabric rolls upright or on wide-diameter cores to prevent permanent creasing in the coated surface
- Allow cold-transported rolls to reach ambient temperature before unrolling to avoid coating micro-cracking at fold lines
- Use PVC-compatible cleaners only; solvent-based products will degrade the knife-coated surface and compromise re-weldability
Before You Request a Quote
Provide the intended deployment environment, including expected temperature range and UV exposure duration, so the coating formulation can be matched to your conditions. Specify the fire safety classification enforced in your destination market — this determines the flame-retardant additive package and the test report you will receive. Indicate whether you require roll stock for your own fabrication line or finished inflatable tent panels with welded seams and access configurations. State your target dimensions, color requirements, and any pattern printing needed for branding or identification.
Frequently Asked Questions
Q: How is the flame-retardant grade verified, and which fire safety standards does the fabric meet?
A: Fire-retardant properties are claimed for this PVC inflatable tent fabric, but the specific grade is confirmed per order based on the standard required in your market. Request the applicable test report — such as DIN 4102, NFPA 701, or local building code classification — before production begins to ensure the additive package and documentation match your site compliance requirements.
Q: What is the test basis for UV resistance claims and extended outdoor deployment?
A: UV resistance is stated as a performance attribute of the knife-coated PVC surface. The specific test method and exposure duration rating are provided in the batch test report. For shelters intended for multi-month outdoor deployment, request the UV weathering data relevant to your climate zone and confirm whether additional surface treatment is recommended.
Q: How is coating weight and adhesion controlled for airtight inflatable performance?
A: Knife-coating applies the PVC compound under controlled blade gap and tension settings, with in-process checks on coating weight uniformity across the web width. Adhesion is verified through peel testing, and finished inflatable panels undergo a minimum 24-hour air pressure retention test to confirm seam and membrane integrity before shipment.
Q: What base fabric denier and weave options are available for inflatable tent applications?
A: Base fabric options are selected based on the structural demands of your inflatable design — higher denier for wind-loaded emergency shelters, lighter constructions for rapidly deployable single-use applications. Provide your inflation pressure and expected wind load data so the appropriate base fabric and coating weight combination can be specified.
Q: How is batch-to-batch color consistency controlled across production runs?
A: Color matching is managed through reference standards maintained in the R&D department, with visual and instrumental comparison at the coating stage. For multi-roll orders intended for a single shelter project, request the batch inspection record showing color evaluation data to prevent visible variation once panels are installed side by side.