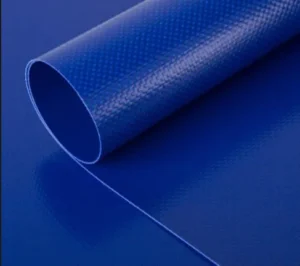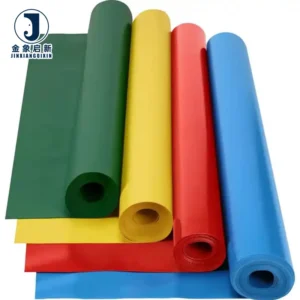
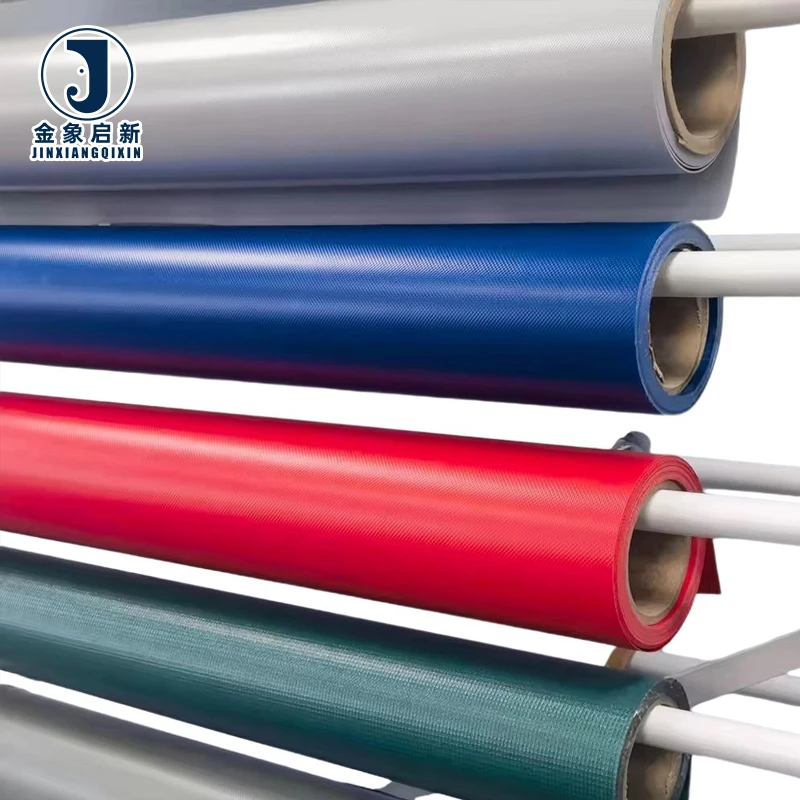
Coating Adhesion Control — Nearly 30 years of PVC coating process refinement ensures predictable peel strength and weld seam integrity across every roll shipped.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PVC Coated Tarpaulin |
| Base Fabric Denier | 1000D |
| Coating Material | PVC |
| Light Blocking | Blackout |
| UV Treatment | Anti-UV (test basis to be confirmed per grade) |
| Flame Retardant | Flame retardant (grade to be confirmed per market requirement) |
| Antibacterial & Mildew Proof | Yes |
| Oil & Stain Resistance | Yes |
| Acid & Alkali Resistance | Yes |
| Temperature Resistance | High temperature and cold resistance (range to be confirmed) |
| Anti-Oxidation | Yes |
| Weather Resistance | Yes |
| Flexibility | Highly flexible, resistant to cracking |
| Self-Cleaning | Yes |
| Welding Compatibility | HF, Hot Air, Sewing |
| Key Features | Blackout, Anti-UV available, Flame Retardant available, Antibacterial, Mildew Proof, Oil & Stain Resistant, Acid & Alkali Resistant, Anti-Oxidation, Weather Resistant, Self-Cleaning |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Event and Exhibition Tents | Complete light control for interior atmosphere, repeated assembly and teardown stress on seams, crowd safety requiring verified flame retardant grade |
| Tensile and Architectural Structures | Sustained structural tension loads, long-term UV and weather exposure, weld seam integrity at stress concentration points |
| Shade Systems and Stadium Canopies | Direct solar exposure demanding UV stability, blackout performance for spectator comfort, wind load resistance across large spans |
| Portable Storage Structures | Abrasion from stored goods, weather sealing against rain ingress, flexibility in cold conditions during winter deployment |
| Airport Hangars and Large Format Textiles | Wide span coverage requiring batch colour consistency, chemical exposure from aviation fluids, fire safety compliance |
Why Coating Weight and Base Denier Together Determine Real Strength
A 1000D base fabric only delivers its tensile potential when the PVC coating penetrates and locks the yarn intersections.
Technical buyers often specify PVC coated tarpaulin roll 1000D by denier alone, assuming the base fabric number guarantees mechanical performance. The reality is that coating weight, coating method and adhesion to the base yarns collectively determine whether tensile and tear values hold under load. A heavy coating on a loosely woven base can mask poor tear propagation resistance, while a thin coating on a dense 1000D weave may leave yarns exposed to abrasion at flex points. [NEED_CITE: relationship between coating adhesion and tensile performance in PVC coated fabrics per ISO 1421]
The failure pattern is consistent: the fabric survives the design load, but the welded seam opens first because the coating did not bond deeply enough into the base fabric structure. This is not a welding machine issue — it is a material specification gap that only shows up after fabrication and installation.
Coating Formulation and Blackout Performance
The blackout capability in this PVC coated tarpaulin roll 1000D is achieved through pigment loading within the PVC coating layers rather than a separate laminated film. This means light blocking performance depends directly on coating weight per side and pigment dispersion uniformity during the coating process. For tent and exhibition fabricators, this matters because inconsistent pigment distribution creates visible light spots when the fabric is backlit — a defect that only appears once the structure is erected and illuminated from inside.
Weld Compatibility Across Joining Methods
This material supports HF welding, hot air welding and sewing, but each method interacts differently with the PVC coating formulation. HF welding relies on the dielectric properties of the PVC layer to generate heat at the interface, and coating thickness directly affects the energy required for a consistent bond. Hot air welding demands that the coating soften uniformly without degrading, which depends on the plasticiser system used. Sewn seams require the coating to remain flexible enough that needle penetration does not initiate crack propagation along the stitch line. [NEED_CITE: HF and hot air welding parameters for PVC coated technical textiles]
How 1000D Denier and Coating Weight Interact
The 1000D base fabric provides the structural skeleton — the yarn thickness and weave density set the upper limit for tensile and tear resistance. However, the PVC coating weight determines how effectively load transfers between yarns at intersection points. Without sufficient coating penetration, individual yarns can pull apart under tear stress even though each yarn alone is strong. This is why two rolls with identical 1000D denier but different coating weights will show markedly different tear propagation behaviour in the field. The total GSM is a combined result of base fabric weight plus coating weight on both sides, and specifying GSM alone without breaking down the base and coating components leaves critical ambiguity in the material definition.
What Happens When Material Specification Gaps Reach the Field
A fabricator receives rolls with the correct 1000D labelling and proceeds to cut and weld. The finished tent or tensile structure passes initial inspection. Weeks later, seams begin to peel at the points of highest flex — not because the welding temperature was wrong, but because the coating adhesion to the base fabric was below the threshold needed for cyclic loading. In another scenario, a batch of blackout tent fabric arrives with slight colour variation between rolls, visible only when panels hang side by side in the finished structure, forcing the contractor to replace entire sections at their own cost. [NEED_CITE: common failure modes in PVC coated fabric installations related to specification gaps]
These outcomes are preventable when the material specification sheet breaks down base fabric denier, coating weight per side, total GSM and treatment grades — and when test reports back the UV and flame retardant claims with the specific standard and grade applicable to the target market.
Why Fabricators Source This Grade Here
Three full production lines with 36 sets of professional coating equipment provide the capacity to hold coating weight and pigment dispersion consistent across every roll in a bulk order — the batch uniformity that tent and tensile structure fabricators depend on.
A 10-person R&D team handles material formulation adjustments, custom width development and sample rolls so fabricators can validate weld settings and colour before committing to full production volume.
Dedicated QA/QC at every production stage, with 100% pre-shipment inspection, catches GSM deviation and coating adhesion variation before the material leaves the facility — addressing the gap between quoted specification and delivered roll.
ISO and CE certified processes with full documentation support, including material specification sheets and test reports where applicable, give fabricators the paper trail their end clients and regulatory bodies require.
Sample rolls developed within days for custom requirements allow fabricators to run HF and hot air weld trials on their own equipment before placing the full order.
Documentation & Verification
- Material specification sheet stating GSM breakdown, 1000D base fabric denier, coating method and weight per side
- Test report for UV resistance — confirm the standard and exposure hours applicable to your market
- Flame retardant grade certificate matching the fire safety classification required for your installation jurisdiction
- Colour reference per roll with batch consistency record across the full order
- Pre-shipment inspection record with GSM and coating weight verification per roll
- ISO and CE certificates included with dispatch documentation
Fabrication, Handling & Storage
- HF weld settings must be calibrated to the specific PVC coating thickness on this 1000D grade before production runs begin
- Hot air welding temperature and speed should be tested on sample offcuts to confirm coating softening without degradation
- Sewn seams on this blackout fabric require UV-stable thread compatible with the PVC coating to prevent stitch line cracking
- Store rolls upright on pallets in a shaded area to prevent flat-spot deformation of the PVC coating surface
- Allow cold-stored rolls to reach ambient temperature before unrolling to avoid coating crack initiation at fold lines
- Clean with mild detergent only — solvent-based cleaners can attack the plasticiser system in the PVC coating layer
What to Include in Your Inquiry
Specify the flame retardant grade required by your local fire safety authority — NFPA 701, DIN 4102, M2, B1 or other — so the correct formulation is matched to your market. Provide the target width, roll length and annual volume to confirm production scheduling and batch consistency allocation. If your fabrication process uses HF welding, state your machine model and typical power settings so weld compatibility can be verified on sample material before the production run.
Frequently Asked Questions
Q: How do you verify the 1000D base fabric denier and GSM match the quotation when the roll arrives?
A: Each roll undergoes pre-shipment inspection where GSM is measured and cross-checked against the material specification sheet. The base fabric denier and coating weight breakdown are documented per roll, not just as a batch average. We provide the inspection record with your shipment so you can reconcile delivered values against your purchase order before fabrication begins.
Q: What flame retardant grade is available and how do I confirm it meets my market requirement?
A: Flame retardant formulations are available in multiple grades. The specific grade must be confirmed against your installation jurisdiction — whether NFPA 701, DIN 4102, M2 or B1 applies. State your target standard in the inquiry and we will match the formulation and provide the corresponding test report with the grade classification documented.
Q: Can I get a sample roll to test HF and hot air weld settings before placing the bulk order?
A: Yes. Sample rolls are developed within days and shipped for fabricators to run weld trials on their own equipment. This allows you to confirm seam strength, coating softening behaviour and blackout consistency under your specific HF or hot air parameters before the full production order is released.
Q: How do you ensure colour and coating consistency across multiple rolls in one shipment?
A: Pigment dispersion and coating weight are monitored at every production stage across the three full production lines. Each roll is logged with its colour reference and coating weight record. The pre-shipment inspection includes a visual and measured comparison across rolls in the same order to flag any deviation before dispatch.