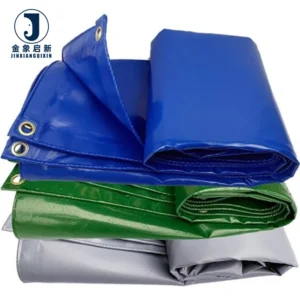
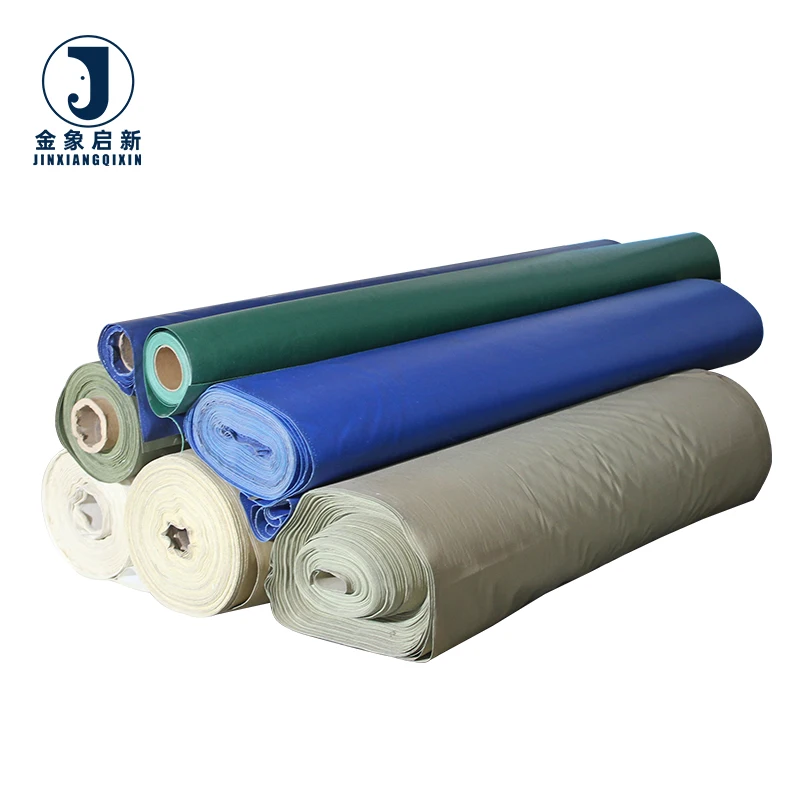
Precision Coating Control — Every roll of PVC Tarpaulin Roll for Awning and Tents is verified against its stated GSM and base fabric specification before dispatch, ensuring fabricators receive the material properties they ordered.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | PVC Tarpaulin Roll |
| Coating Material | PE (HDPE weaving with LDPE lamination on both sides) |
| Weight (GSM) | 50gr/m2 ~ 220gr/m2 available (range covers product family — confirm the grade for this item) |
| Total Thickness | 0.2-0.4mm / 8 mil-16 mil / Custom |
| Color Options | Blue, Blue/Orange, Green, Grey, Black, Clear, Grey/Green, Orange, or custom |
| Waterproof | Yes |
| Tear Resistance | Tear resistant construction |
| UV Treatment | Available (test basis not stated in source) |
| Anti-Mildew | Mildew proof and anti-aging |
| Custom Printing | Available |
| Certifications | ISO, CE (specific standard numbers not stated in source) |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Awning fabrication | Prolonged UV exposure, wind loading on frame structures, repeated deployment and retraction cycles |
| Tent manufacturing | Weather exposure across seasons, tension at pole contact points, weld integrity at panel seams |
| Outdoor weather protection covers | Rain and moisture contact, mildew risk in humid storage, handling abrasion during placement |
| Transportation and storage wraps | Road dust and debris, tie-down strap friction, sun exposure during transit |
Why the Quoted GSM Does Not Match the Roll You Receive
Coating weight and base fabric density must be verified independently, not assumed from a single GSM figure.
Tarpaulin buyers across Southeast Asia and Africa regularly open containers to find material that feels lighter and performs below expectation. The GSM printed on the quotation often reflects a product family range rather than the specific roll grade shipped. When HDPE weave density and LDPE lamination thickness are not separated on the specification sheet, there is no baseline to verify against [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421]. Fabricators cutting panels for awnings and tents discover the shortfall only after seams fail under wind load or panels sag between frame points. This PVC Tarpaulin Roll material coating technology discussion starts with the understanding that weight alone is a poor proxy for structural performance.
Lamination Adhesion and Seam Welding Behaviour
PE-laminated tarpaulin relies on thermal bonding between the LDPE coating layers and the HDPE woven substrate. The adhesion strength at this interface determines whether a heat-welded seam holds under tension or delaminates at the flex point. PVC Tarpaulin Roll stock with insufficient coating penetration into the weave structure will separate before the base fabric itself fails. Fabricators running hot-air or impulse welders must confirm the lamination method and coating weight per side, not just the total GSM, to set correct temperature and dwell time parameters.
Base Fabric Denier and Weave Density Under Load
The HDPE woven base fabric carries the structural load in any tarpaulin installation. Denier and thread count per inch define how stress distributes across the panel when wind presses against an awning face or a tent wall. A lighter weave may accept lamination adequately but propagate tears rapidly once a puncture or cut edge initiates failure. Technical buyers specifying PVC Tarpaulin Roll for load-bearing membrane structures should request the base fabric specification alongside the coating weight [NEED_CITE: relationship between base fabric denier and tear propagation in coated fabrics]. This material-level data allows accurate comparison between suppliers quoting similar GSM ranges.
Interpreting Thickness, Coating Weight, and Colour Consistency
Total thickness of 0.2-0.4mm in laminated PE construction reflects the combined profile of the HDPE weave and both LDPE lamination layers. This measurement correlates with puncture resistance but does not directly indicate tensile strength, which depends more heavily on base fabric density. When ordering multiple rolls for a single awning or tent production run, colour consistency between rolls becomes critical — panels installed side by side reveal even minor pigment variation. The lamination process must maintain uniform coating temperature and pressure across the full production batch to prevent gloss and shade drift. Specifying PVC Tarpaulin Roll material coating technology parameters by written standard rather than verbal description reduces this batch-to-batch variance significantly.
The Hidden Cost of Specifying on GSM Alone
When a tent manufacturer selects material based solely on a quoted weight figure, the finished structure may underperform in the field without any obvious manufacturing defect. Coating weight that falls below the expected threshold reduces stiffness and dimensional stability, causing awning panels to pool water rather than shed it. Welded seams on underweight material delaminate under cyclic wind loading because the LDPE layer lacks sufficient thickness to form a continuous bond across the joint [NEED_CITE: coated fabric seam peel strength testing methods]. The cost of replacing failed structures in the field — including labour, logistics, and reputational damage — consistently exceeds the savings from accepting lighter material. Batch colour variation compounds the problem when replacement panels do not match the original installation.
Why Fabricators Source This Material Here
Three full production lines and 36 sets of professional equipment support consistent lamination quality across high-volume roll orders for awning and tent applications. A dedicated 10-person R&D team handles material selection and sample development, allowing fabricators to receive test rolls within days rather than weeks. Every production stage includes QA/QC checkpoints, with 100% inspection before shipment verifying GSM, colour reference, and coating adhesion against the specification sheet. The facility’s ISO and CE certification framework supports documentation requirements for export markets across multiple regulatory regions. Custom width, colour, and printing options carry realistic lead times and minimum quantities suited to production planning rather than speculative stockholding.
Documentation & Verification
- Material specification sheet stating confirmed GSM, base fabric denier, and LDPE lamination method per roll
- UV treatment test report with stated standard and exposure duration where applicable
- Pre-shipment inspection record confirming weight, colour, and coating adhesion across the batch
- Roll packing list with individual roll identification for traceability
- Certificate of origin and customs documentation for export clearance
Fabrication, Handling & Storage
- Set hot-air welder temperature to match LDPE lamination melting range; test on offcut before production runs
- Store rolls horizontally on padded racks to prevent creasing through the HDPE weave core
- Allow rolled material to acclimatize before unrolling in cold conditions to avoid lamination cracking
- Use sharp rotary blades for cutting to prevent fraying at HDPE weave edges before welding
- Clean finished awning panels with mild detergent only; solvents may degrade the LDPE surface layer
Specifying Your Material Requirements
Provide the intended application, panel dimensions, and structural loading expectations so the correct grade within the available GSM range can be recommended. Specify any UV treatment or fire-retardant requirement along with the compliance standard applicable in your target market. Indicate whether you need rolls at standard width or custom dimensions, and confirm colour references with physical samples before full production commitment.
Frequently Asked Questions
Q: What is the difference between PVC-coated and PE-laminated tarpaulin at the material level?
A: PVC-coated tarpaulin uses a knife-coating or calendering process where liquid PVC bonds directly into the polyester base fabric, creating strong adhesion suitable for high-frequency welding. PE-laminated tarpaulin bonds pre-formed LDPE film to an HDPE woven substrate through heat and pressure. The lamination method generally produces lighter material at comparable GSM, with different thermal welding parameters required at fabrication.
Q: How is GSM measured and how does it relate to tensile and tear strength?
A: GSM represents the total weight per square metre of the finished fabric including base cloth and all coating or lamination layers. Tensile and tear strength depend primarily on the base fabric denier and weave density, not the coating weight. Two rolls at identical GSM can show significantly different strength values if one uses a heavier base fabric with lighter coating and the other reverses that ratio.
Q: Can you provide a third-party test report for UV and flame-retardant treatment?
A: UV treatment and flame-retardant grades are available across the product range. Request the specific test standard applicable to your market — such as exposure duration and evaluation method for UV stability, or classification level for fire performance — and confirm the grade before placing a bulk order. Documentation is supplied with the test basis clearly stated.
Q: How do you control colour consistency between rolls in the same order?
A: Colour consistency is maintained through controlled LDPE lamination temperature, consistent pigment dosing, and continuous process monitoring across the production run. Physical samples from the production batch are available for approval before dispatch. Rolls within a confirmed order are produced in a single campaign to minimize inter-batch variation once panels are installed side by side.
Q: What welding method is recommended for PE-laminated tarpaulin?
A: Hot-air welding and impulse heat sealing are both suitable for PE-laminated HDPE tarpaulin. The LDPE lamination layer melts at a lower temperature than PVC, requiring adjusted welder settings. Seam strength depends on coating thickness per side and lamination adhesion to the base weave. Always run test welds on production offcuts to confirm peel strength before committing to full panel fabrication.