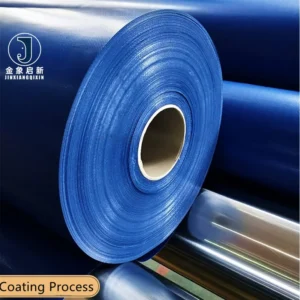
Precision Coating Control — Each roll of 650GSM 1000D1000D 2323 1.50*50M/R is verified against the stated coating weight at multiple production stages, ensuring technical buyers receive material that matches the specification sheet, not just the quotation label.
Technical Specifications
| Parameter | Value |
|---|---|
| Specification | 650GSM 1000D1000D 2323 1.50*50M/R |
| Product Type | PVC Coated Tarpaulin Roll |
| Base Fabric Denier | 1000D × 1000D polyester |
| Weave Density | 23 × 23 threads per inch |
| Coating Material | PVC |
| Surface Finish | Glossy (matte option available) |
| Roll Width | 1.50 m |
| Roll Length | 50 m |
| Temperature Range | -15ºC to 70ºC |
| UV Treatment | Customised — confirm grade required for your market |
| Flame Retardant | Available in flame retardant grades — confirm the grade required for your market |
| Anti-Fungal | Treated (standard not stated) |
| Waterproof | Fully waterproof PVC coated construction |
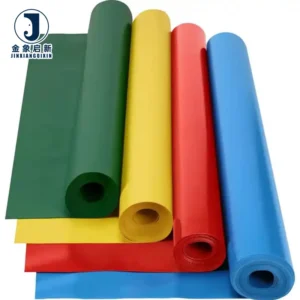
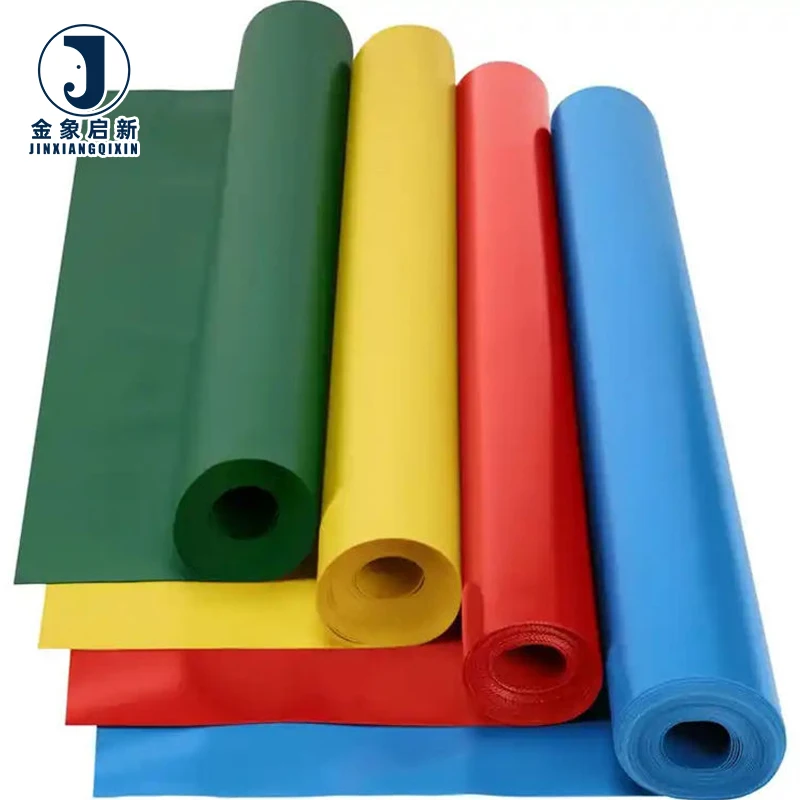
| Colour Options | Blue, Yellow, Black, Green, White, Custom |
| Working Life | 3–10 years depending on usage environment |
| Standards | ISO 14001, ISO 45001, CE, RoHS |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Truck and trailer side curtains | Constant flexing at hinges, road abrasion, UV exposure, high-frequency welding at seams |
| Construction site and equipment covers | Prolonged sun exposure, wind load, rain ingress, puncture from sharp structural edges |
| Tent and awning panels | Repeated folding and tensioning, solar heat gain, seam integrity under load |
| Inflatable and membrane structures | Internal air pressure, sustained UV, thermal expansion cycles, welded joint integrity |
| Multi-purpose protective covers | General weather exposure, handling abrasion, stacking loads on pallets |
Why 650GSM Alone Does Not Guarantee Fabric Strength
Tensile and tear resistance depend on how coating weight and base fabric denier work together, not on the GSM figure printed on the label.
When a technical buyer specifies PVC coated tarpaulin 650 gsm, the expectation is that the material will withstand the mechanical loads of its intended application. Yet GSM is a combined measure — base fabric plus coating — and two rolls carrying the same GSM label can perform very differently if one achieves the figure through a heavier coating on a lighter scrim while the other uses a denser base fabric with a thinner coat. [NEED_CITE: tensile and tear test methods for coated fabrics per ISO 1421]. The 1000D × 1000D polyester scrim in this roll provides the structural skeleton; the PVC coating locks the weave in place and supplies environmental resistance. Specifiers who examine only the total weight risk selecting material that is coating-heavy but scrim-light, which tears more easily once a nick propagates through the weave.
How Base Fabric Denier Shapes Mechanical Behaviour
The 1000D × 1000D yarn count in both warp and weft directions establishes the load-bearing backbone of this PVC coated tarpaulin 650 gsm. Denier defines the linear mass of each filament bundle — higher denier yarns carry greater individual filament strength. Because the yarns in both directions are matched at 1000D, the fabric exhibits balanced biaxial tensile properties, reducing the risk that one direction yields before the other under uneven loading such as wind gusts on a tensioned membrane.
Mesh Density and Its Role in Dimensional Stability
The 23 × 23 weave density means 23 threads per inch in both warp and weft. This mesh count places the fabric in the higher-density bracket for its weight class. A denser weave restricts yarn migration under tension, which directly benefits fabricators who rely on consistent dimensional behaviour during high-frequency welding or hot-air seaming. When mesh count is too low, individual yarns can shift under the welding bar, producing uneven seam thickness and increasing the likelihood that a weld fails before the fabric itself reaches its service limit.
Surface Finish and Welding Compatibility
The glossy surface finish on this roll promotes strong initial wetting when solvent-based adhesives are used, and it responds predictably to high-frequency welding because the smooth PVC layer melts uniformly across the seam interface. Matte finish, available as an alternative, introduces a micro-textured surface that diffuses light reflection and can reduce visible scuffing in field applications. Fabricators switching between glossy and matte within a single project should recalibrate welding temperature and dwell time parameters, as the surface texture influences heat transfer rate at the interface. [NEED_CITE: high-frequency welding parameters for PVC coated polyester fabrics].
Reading the Specification Sheet Beyond the GSM Number
GSM tells you total areal weight, but a complete material specification requires understanding each contributing layer. The 650GSM figure on this roll is the sum of the 1000D × 1000D polyester scrim and the PVC coating applied to both faces. The 23 × 23 mesh count indicates how tightly those yarns are woven before coating, which governs the amount of PVC that penetrates the interstices versus remaining on the surface. Higher penetration improves coating-to-scrim adhesion but can stiffen the hand of the fabric. The -15ºC to 70ºC operating temperature range reflects the plasticiser formulation used in the PVC compound — at the lower boundary, the material retains sufficient flexibility to avoid brittle cracking when folded or tensioned in cold conditions, while at the upper boundary the coating resists tackiness and sagging under sustained solar loading.
The Cost of Specifying on GSM Without Verifying the Substrate
Procurement decisions based solely on total weight create downstream failures that surface only after installation. A coating-heavy roll may pass the weight check yet tear rapidly once a cut edge is exposed to cyclic wind loading. A scrim-light fabric can delaminate at welded seams because the PVC coating carries the weld but the underlying yarns lack the strength to hold the joint under tension. [NEED_CITE: coated fabric delamination failure modes under cyclic mechanical stress]. Batch-to-batch variation in coating weight compounds the problem — one roll may test within tolerance while the next falls below, and the difference becomes visible only when two panels are installed side by side and one sags under its own weight.
Why Material Buyers Source This Roll Here
Three full production lines with 36 sets of professional coating equipment allow the facility to maintain tight GSM tolerance across long production runs, which matters when a single order spans multiple rolls that must match in weight and colour.
A 10-person R&D team develops custom colour samples within days, enabling fabricators to confirm shade consistency before committing to full batch production rather than discovering colour drift after delivery.
Dedicated QA/QC at every production stage, with 100 percent pre-shipment inspection, means each roll of this PVC coated tarpaulin 650 gsm is checked for coating weight, surface defect, and dimensional accuracy before it leaves the factory.
The coating process controls — from scrim tensioning to knife-over-roll application — are calibrated to this specification, so buyers who reorder receive material that matches their approved sample.
Documentation & Verification
- Material specification sheet stating GSM breakdown by base fabric and coating weight for this exact roll configuration
- UV and flame retardant test reports issued against the specific grade selected — confirm required standard before production
- Pre-shipment inspection record documenting coating weight, surface quality, and roll dimensions
- Roll packing list with individual roll weights and dimensions for receiving verification
- Certificate of origin and customs documentation supporting export to your market
Fabrication, Handling & Storage
- High-frequency welding on the glossy 650GSM surface typically requires standard PVC parameters — recalibrate when switching to matte finish
- Cut edges on the 1000D × 1000D scrim should be sealed or hemmed to prevent yarn pull-out under cyclic load
- Store rolls horizontally on racking to prevent permanent creasing across the 1.50 m width
- Allow cold-stored rolls to acclimate before unrolling to avoid surface cracking below the -15ºC threshold
- Solvent-based adhesives bond well to the glossy PVC surface — test adhesion on matte finish before production
- Plan panel layouts to minimise weld seams running parallel to the 50 m roll length for improved flatness
Specifying the Right Material for Your Project
Technical buyers and fabricators evaluating this PVC coated tarpaulin 650 gsm should provide the intended application and exposure conditions, including any UV or flame retardant grade required by local regulation. Specify whether rolls are needed in standard 1.50 m width or a custom width, the required surface finish, and whether colour matching against an approved reference sample is necessary. Indicate annual volume to confirm production scheduling and batch consistency provisions.
Frequently Asked Questions
Q: How is 650GSM measured — is it total weight or coating only?
A: The 650GSM figure represents total areal weight, combining the 1000D × 1000D polyester scrim and the PVC coating on both faces. A material specification sheet is supplied with each order that breaks down the contribution of base fabric and coating separately, allowing buyers to verify the substrate proportion independently of the total weight.
Q: Can you supply a test report for UV and flame retardant treatment with each batch?
A: UV and flame retardant treatments are available in various grades. Provide the standard required by your market — such as DIN 4102, NFPA 701, or a regional equivalent — and the corresponding test report will be issued for the specific grade produced. Confirm the required certification level before production begins to ensure compliance documentation accompanies the shipment.
Q: What is the difference in weld performance between glossy and matte surface?
A: The glossy surface provides uniform heat transfer during high-frequency welding, producing consistent seam strength with standard PVC welding parameters. Matte finish introduces surface texture that can alter heat distribution, often requiring adjustment of temperature or dwell time. Fabricators should run a short test weld when switching finishes to validate seam integrity.
Q: How do you guarantee colour consistency across multiple rolls in one order?
A: Rolls within a single production batch are manufactured from the same PVC compound mix and base fabric lot. Pre-shipment inspection includes visual comparison against the approved reference sample. For orders requiring strict colour matching across multiple batches, request production samples from each run before full quantity is dispatched.
Q: What base fabric options exist if I need different tensile strength requirements?
A: The 650GSM roll described here uses a 1000D × 1000D scrim at 23 × 23 mesh. For applications requiring higher tensile or tear values, alternative base fabric deniers and weave densities are available — provide your target strength specification and the R&D team will recommend the appropriate scrim configuration and coating weight combination.