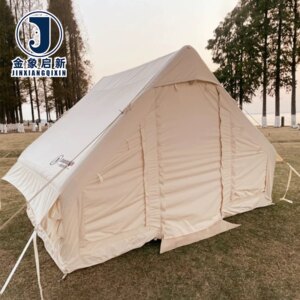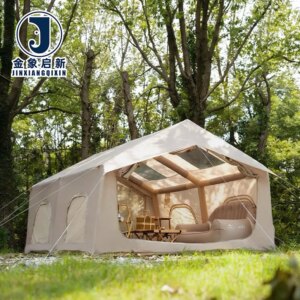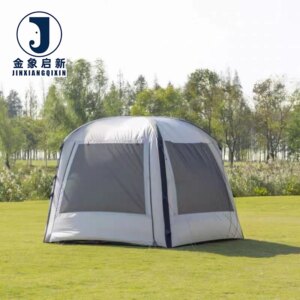
Deep Process Control Over Coating Weight — nearly three decades focused on PVC coated fabric, with measurable adhesion and GSM verification applied to every inflatable tent fabric roll before dispatch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Inflatable Tent Fabric |
| Core Material | PVC Tarpaulin |
| Coating Method | Knife Coated |
| Capacity Reference | 2-8 Person Tent Structures |
| Key Features | Waterproof, Windproof, Tear-resistant |
| UV Resistance | Available in UV-resistant grades — confirm the grade required for your market |
| Design Format | Single Layer Construction |
| Construction Style | Four-Season, Quick Automatic Opening |
| Customization | OEM & ODM — Material Selection and Product Design |
| Quality Control | Full-process Inspection with Dedicated QA&QC Staff |
| Certifications | ISO9001, ISO14001, ISO45001, CE |
Application Suitability
| Application | Exposure & Requirement |
|---|---|
| Emergency relief stations for disaster response | Rapid deployment, sustained rain and wind exposure, repeated inflation cycles, transport abrasion |
| Mobile command centers at infrastructure sites | Continuous outdoor weathering, UV exposure, frequent setup and teardown, ground contact abrasion |
| Temporary storage shelters at construction sites | Long-term weather exposure, dust and debris ingress prevention, wind load on inflated structure |
| Industrial logistics and engineering management hubs | Semi-permanent inflated structures, forklift and equipment proximity, temperature fluctuation |
Why Coating Weight Matters More Than Stated GSM for Inflatable Tent Fabric
A specification sheet that lists GSM without separating base fabric weight from coating weight leaves buyers unable to verify what actually arrived on site.
When procurement teams source inflatable tent fabric by total GSM alone, they often discover after delivery that the coating layer is thinner than expected while the base fabric carries more weight than necessary. The coating is what delivers waterproof and windproof performance in an inflated structure. A base-heavy fabric with minimal PVC coating will show adequate tensile numbers on paper but fail to hold air pressure consistently across welded seams. [NEED_CITE: relationship between coating weight and seam peel strength in PVC tarpaulin per ISO 1421 test methods] I have seen project specifications accepted at quotation stage only for the delivered rolls to underperform during inflation testing because the coating adhesion was insufficient for the seam geometry required by the tent design.
How Knife Coating Delivers the Adhesion Needed for Inflated Structures
The knife coated process applied to this inflatable tent fabric forces PVC paste directly into the base fabric weave under controlled blade pressure, producing a mechanical bond between coating and yarn. This matters for inflatable tent structures because the fabric undergoes constant internal pressure and cyclic flexing every time the tent is inflated and deflated. A laminated or calendar-coated alternative may separate at the coating-to-fabric interface under these repeated stress cycles.
Base Fabric Denier and Weave Density Define Tear Propagation Behaviour
The denier of the yarns and the warp-weft density of the base fabric govern how a puncture or cut propagates once the inflatable structure is under pressure. A tighter weave with higher-denier yarns resists tear extension across the panel, which is critical when an inflatable tent is deployed on rough terrain or near construction equipment. The single layer construction relies entirely on this base fabric integrity because there is no secondary layer to arrest a running tear. [NEED_CITE: tear propagation test methods for coated fabrics per DIN 53363]
Reading GSM Correctly When Specifying Inflatable Tent Material
Total GSM on a PVC tarpaulin data sheet combines the base fabric weight and the coating weight, but these two components serve different functions in an inflatable tent application. The base fabric provides tensile and tear strength, while the PVC coating delivers waterproofing, wind resistance, and the surface necessary for heat-welded seams. Two fabrics can share the same total GSM yet perform very differently if one allocates more weight to coating and less to base yarn. Buyers specifying inflatable tent fabric should request a breakdown showing base fabric weight and coating weight separately, then cross-reference these values against the seam peel strength data for the welding method their fabricator uses. The four-season design intent of this material means it must maintain coating flexibility and adhesion across a wide temperature range without becoming brittle in cold deployment or overly soft in direct sun.
The Cost of Specifying Inflatable Tent Fabric on Price Per Kilogram Alone
When buyers select material based on cost per kilogram without verifying the coating-to-base ratio, the delivered rolls may carry the correct total weight but with a thinner PVC layer than the inflatable structure demands. This shows up first at the welded seams during inflation testing — the seam peels before the fabric body reaches its rated pressure. In disaster response procurement, this failure mode delays deployment and forces emergency re-sourcing. Batch-to-batch coating inconsistency compounds the problem, as the same welding temperature and dwell time that worked on the first roll may underperform on the next. [NEED_CITE: weld seam peel failure modes in PVC coated fabrics under cyclic pressure loading]
What the Production Process Brings to This Material
Three full production lines and 36 sets of professional equipment support the volume required for large-scale inflatable tent fabric orders without splitting a single order across different coating machines, which preserves batch consistency in coating weight and colour. The 10-person R&D team handles material selection and sample development specific to inflatable structure requirements, producing customised samples within days so buyers can run weld tests before committing to bulk. A dedicated QA and QC team inspects every production stage, with 100% pre-shipment inspection verifying that the GSM, coating adhesion, and colour match the approved sample. ISO9001, ISO14001, ISO45001, and CE certifications are maintained and documentation is provided per shipment. [NEED_CITE: ISO 9001 quality management requirements for coated fabric manufacturing] Full OEM and ODM capability allows buyers to specify base fabric denier, coating weight, and surface finish rather than accepting a stock grade that may not suit their inflatable tent design.
Documentation & Verification
- Material specification sheet stating GSM, base fabric weight, and coating weight per batch for inflatable tent fabric
- UV-resistant and flame-retardant test reports tied to specific production batch numbers where applicable
- ISO9001, ISO14001, ISO45001, and CE certificates provided with each shipment
- Pre-shipment inspection record confirming coating adhesion and colour consistency before dispatch
- Certificate of origin and customs documentation for cross-border inflatable tent fabric procurement
Fabrication, Handling & Storage
- Heat weld parameters must be adjusted to the specific coating weight of this knife coated PVC tarpaulin to prevent seam peel
- Store rolls horizontally on pallets to avoid permanent creasing in the PVC coating layer
- Allow cold-stored rolls to reach ambient temperature before unrolling to prevent coating crack at low temperature
- Use PVC-compatible cleaners only to avoid dissolving the knife coated surface finish
- Plan panel cutting layout to minimise weld seams across high-stress zones of the inflatable structure
What to Include with Your Inquiry
To receive an accurate inflatable tent fabric specification and quotation, provide the intended deployment environment including typical wind and rain exposure, the inflation pressure your tent design operates at, and the welding method your fabricator uses. If your market requires specific fire classification or UV treatment, state the standard or grade so the correct formulation is quoted. Indicate whether you need rolls in stock widths or custom widths, and whether you require finished cut panels or raw roll stock.
Frequently Asked Questions
Q: What base fabric denier and coating weight are used for this inflatable tent fabric grade?
A: The base fabric denier and coating weight are configured to the buyer’s specification under our OEM and ODM service. We provide a material specification sheet stating the exact base fabric weight and coating weight per batch, so you can verify the composition matches your inflatable tent design requirements before production begins.
Q: How is UV resistance measured and what test standards apply?
A: UV-resistant treatment is available in multiple grades depending on your deployment climate and expected exposure duration. We provide test reports tied to specific batch numbers — confirm the grade and test standard required for your target market so we can supply the matching formulation and documentation.
Q: What is the seam weld strength compared to the fabric body tensile value?
A: Weld seam strength depends on the coating weight, welding temperature, and dwell time used by your fabricator. We supply coating adhesion data and recommend weld parameters matched to the specific knife coated PVC tarpaulin grade ordered, enabling your production team to achieve reliable seam performance in inflatable structures.
Q: Can flame-retardant treatment be specified and certified per batch?
A: Flame-retardant grades are available and can be specified at inquiry stage. We supply test reports linked to the batch number of your inflatable tent fabric delivery, confirming the treatment level. State the fire classification standard required for your market so the correct grade is formulated and documented.
Q: How does single-layer PVC construction compare to multi-layer alternatives for inflatable tents?
A: Single layer construction reduces weight and packed volume, which matters for rapid deployment in emergency relief and remote construction sites. The knife coated PVC tarpaulin achieves waterproof and windproof performance through coating integrity rather than relying on a secondary layer, simplifying fabrication and reducing the number of weld seams in the finished inflatable structure.